ENEnglish
 VITiếng Việt
 ZH中文
 KO한국어
 JA日本語
 FRFrançais
 ITItaliano
 PTPortuguês
 ESEspañol
 HEעברית
 ARالعربية

 certificates
Incoming material
Mill certificates checked; grade, size, thickness and surface verified – see steel sourcing.
Solution · Quality control
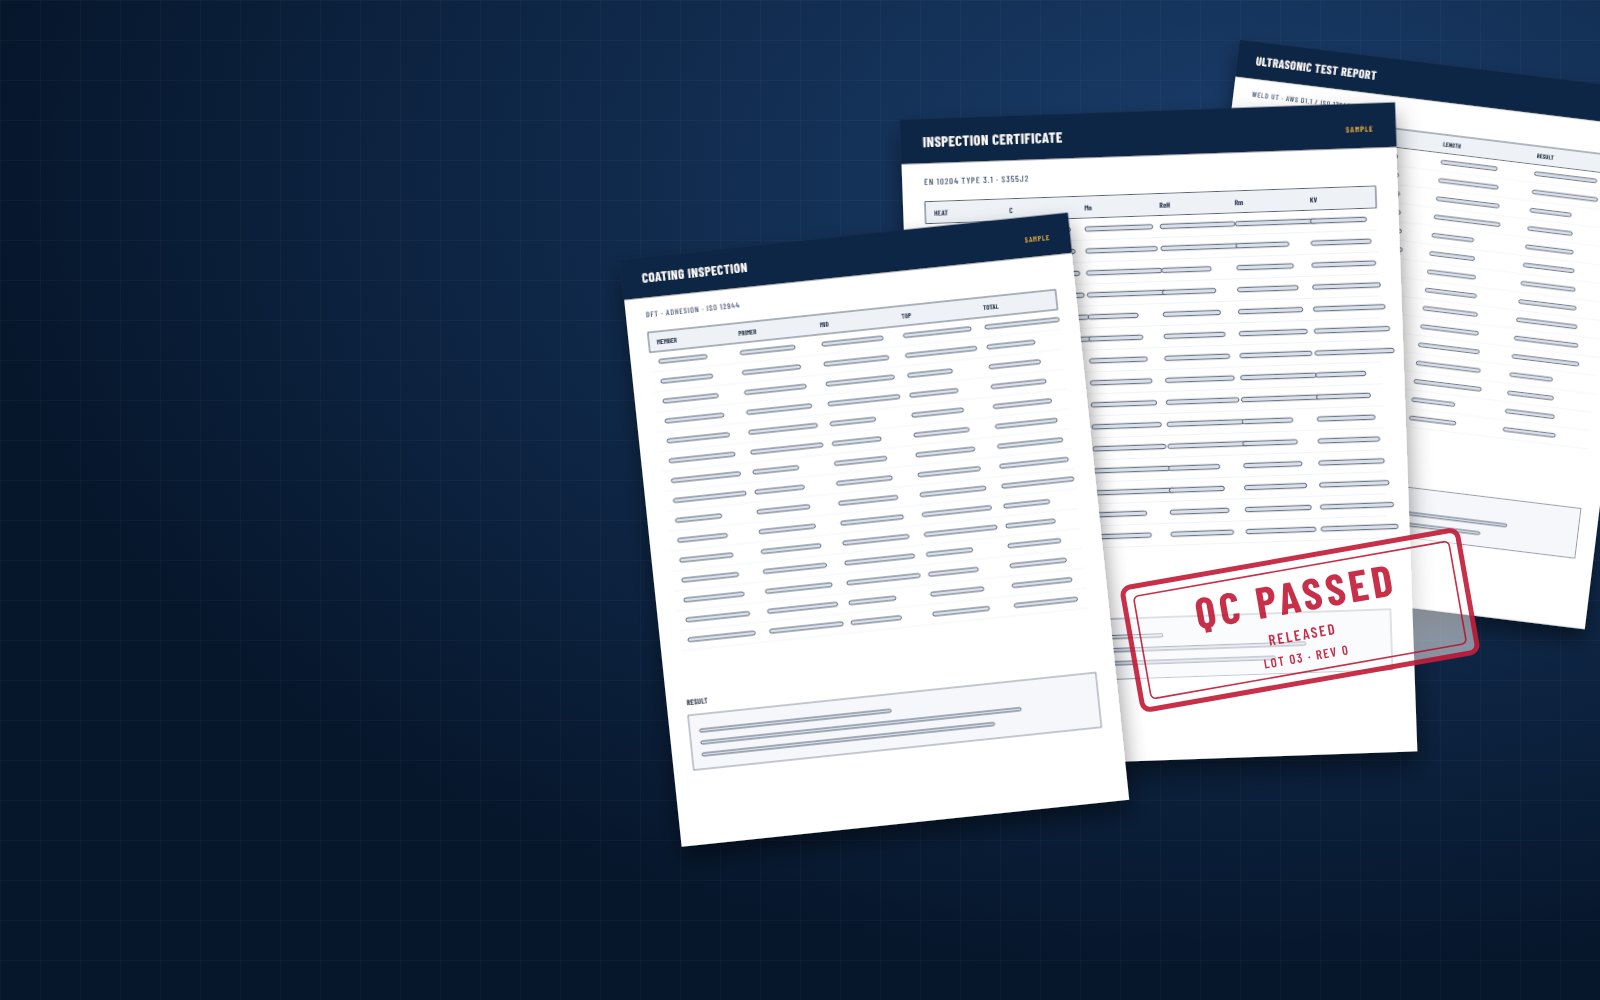
An inspection and test plan for every project, inspection at every stage from incoming steel to packing, full traceability from the mill heat to the piece on site, and a complete manufacturing data record (MDR) handed over with the structure – under certified fabrication and welding systems.
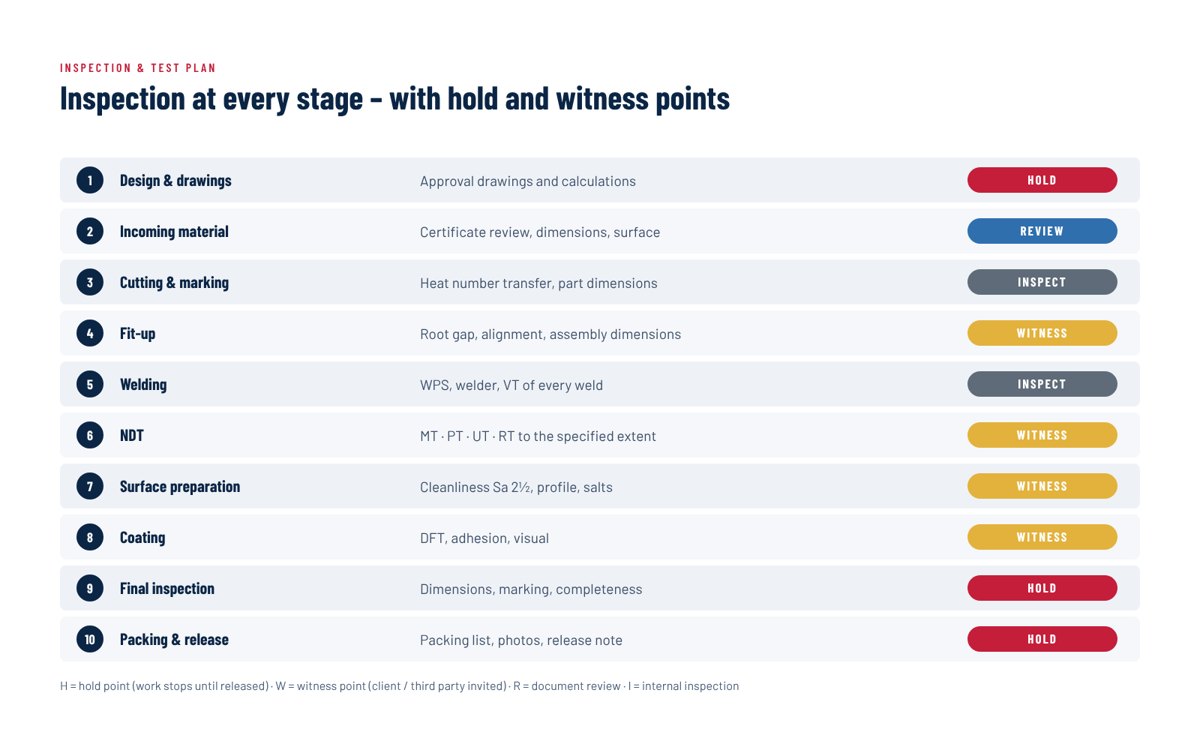
Quality in steel fabrication is not a slogan – it is a plan, a set of inspections and a paper trail. Every World Steel project starts with an inspection and test plan (ITP) that lists each activity, the standard it is checked against, who checks it and where your inspector is invited to witness or must release the work.
Our fabrication and welding systems are certified – ISO 3834-2 for welding quality, EN 1090-2 EXC3 with CE marking, AS/NZS 5131 construction category CC3 and IAS AC472 for structural steel fabricators – and every inspection result is recorded in the manufacturing data record handed over with the structure.
Inspection stages
From the mill certificate to the container door.
certificates
Mill certificates checked; grade, size, thickness and surface verified – see steel sourcing.
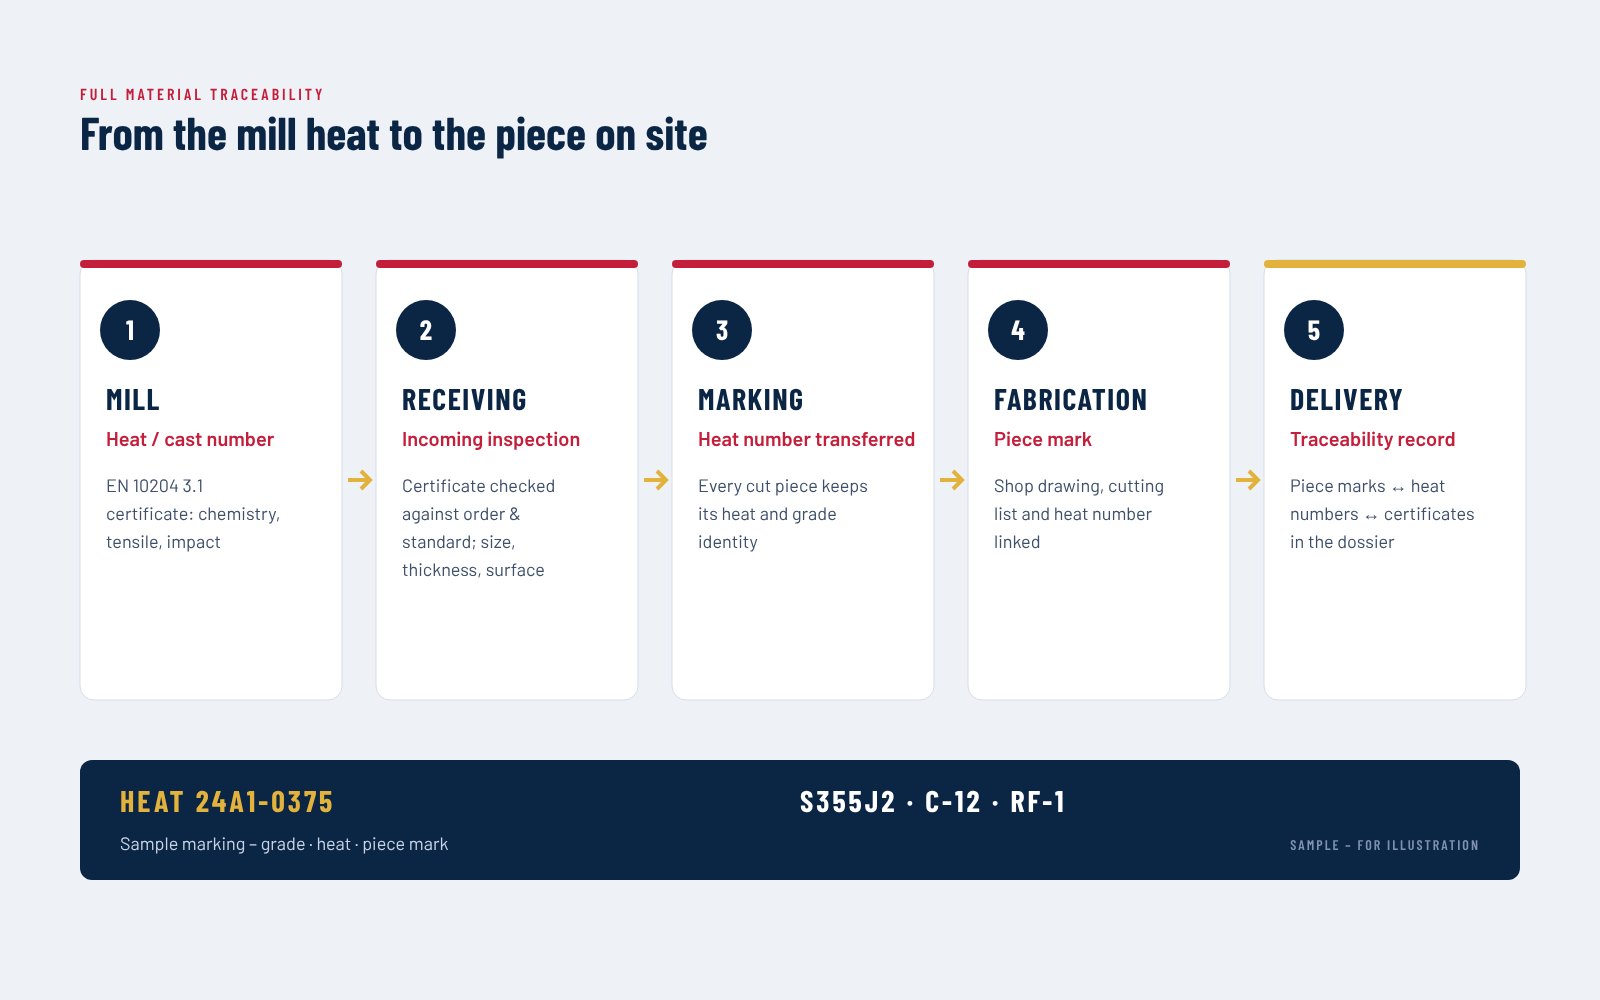 heat → piece
Heat numbers transferred to every part and linked to piece marks and drawings.
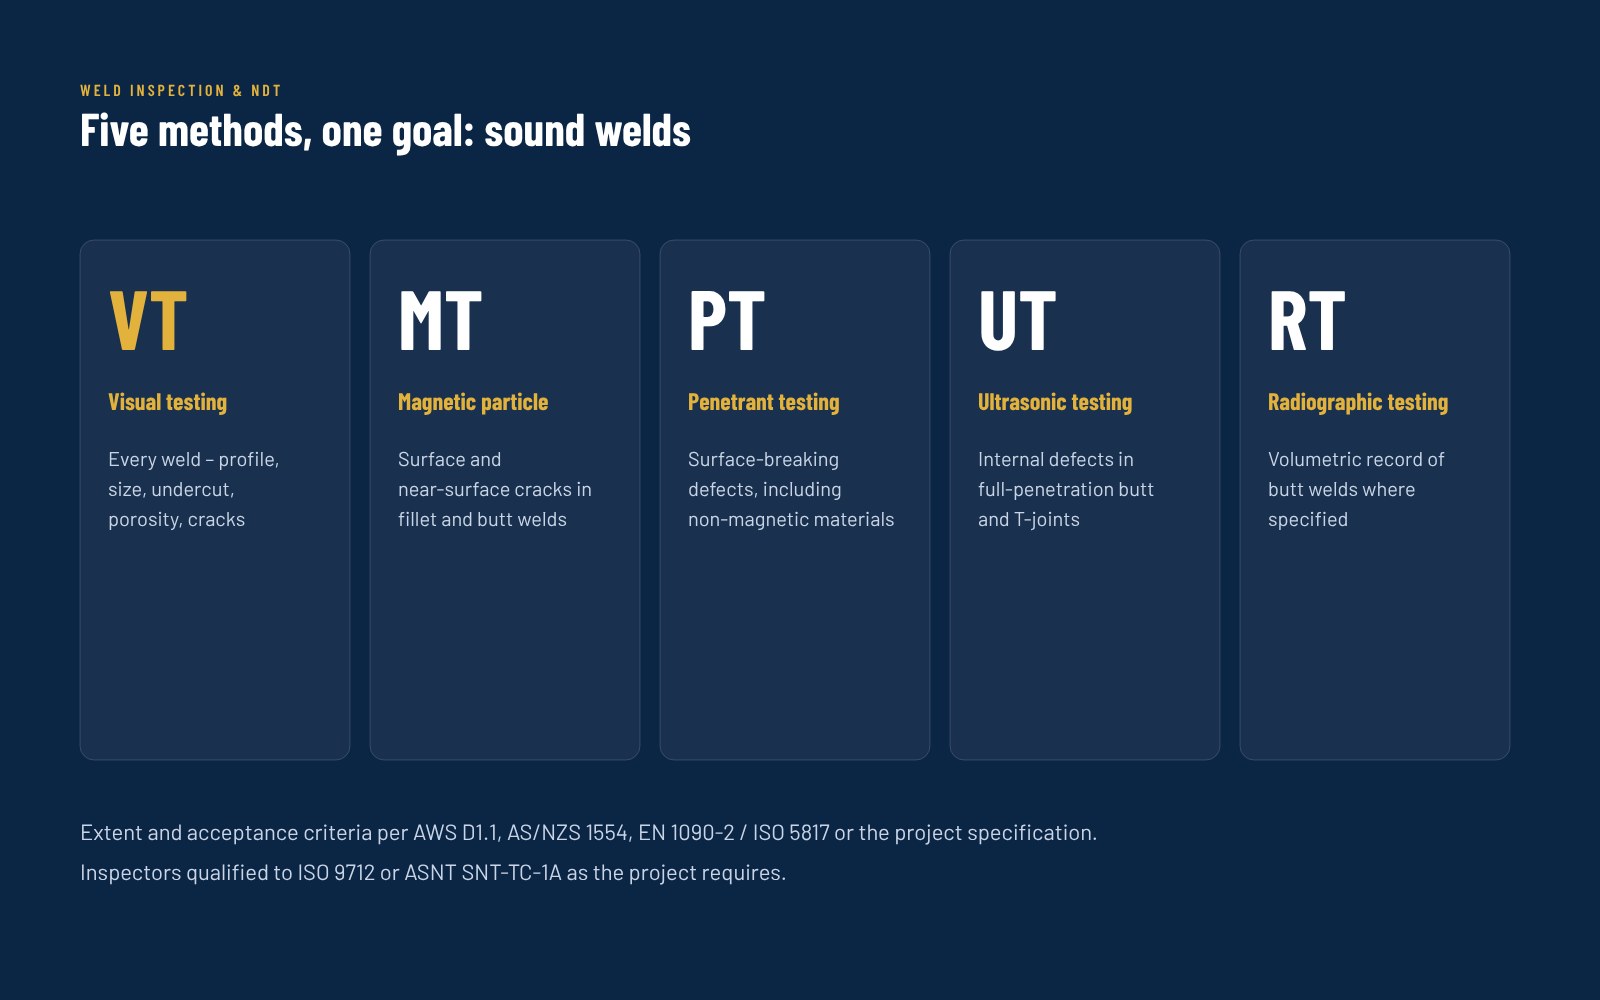 VT · MT · PT · UT · RT
Procedures, welder qualification, visual inspection of every weld and NDT as specified.
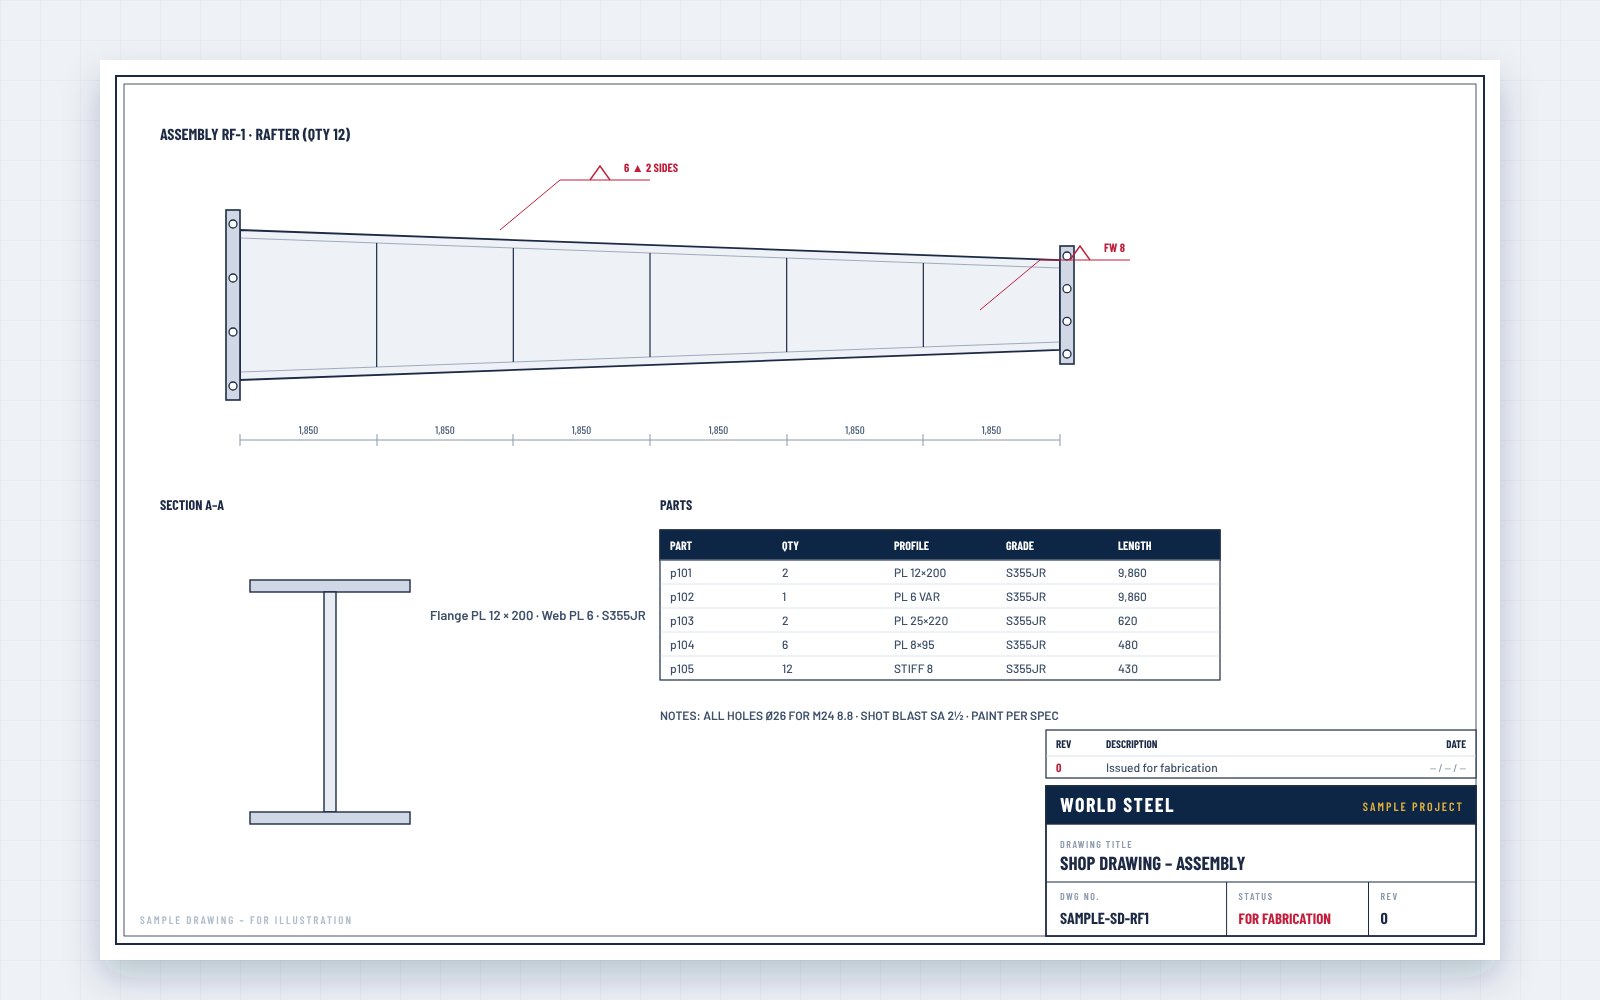 fit-up · trial assembly
Assemblies checked against the released shop drawings; trial assembly where required.
 Sa 2½ · DFT
Blast cleanliness, profile, dry-film thickness and adhesion recorded for every lot.
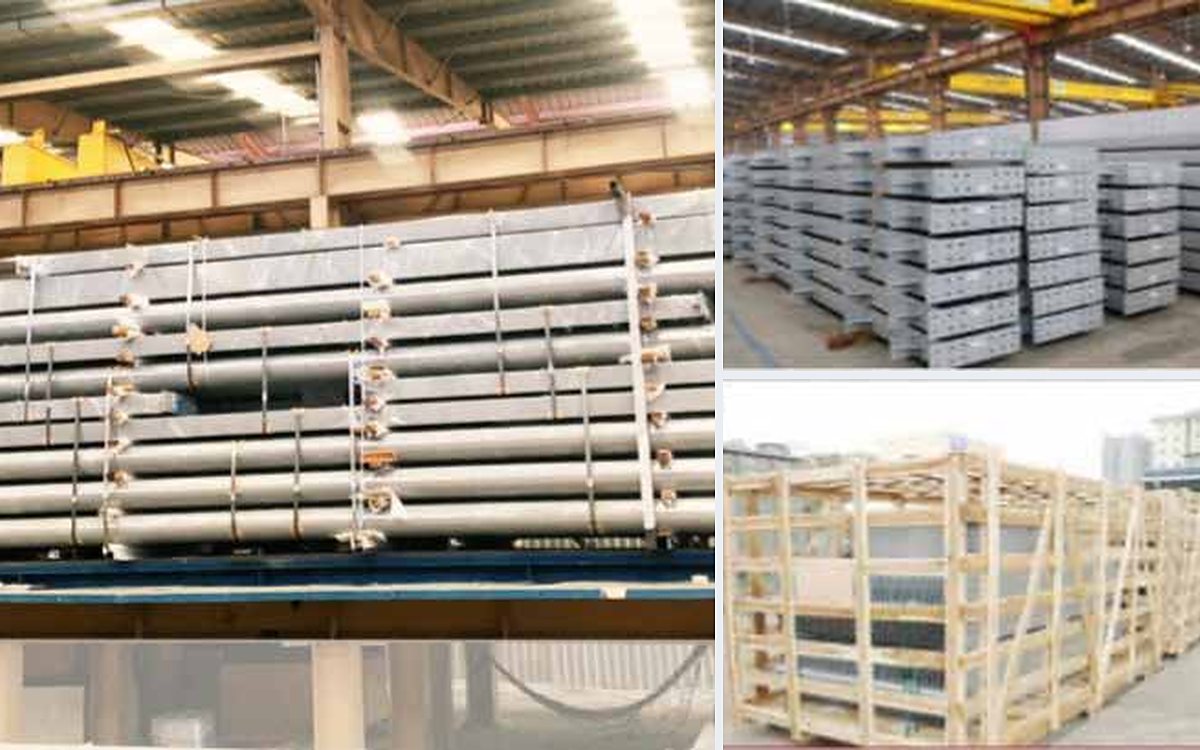 release
Marking, completeness and packing checked; release note issued – see export packing.
Aplicaciones
A project ITP with hold, witness and review points – agreed with you before fabrication.
EN 10204 3.1 certificates checked against the order and the standard on receipt.
Heat numbers carried to every cut piece and linked to piece marks.
Qualified procedures (WPS/PQR) and welders; every weld visually inspected.
MT, PT, UT and RT by qualified inspectors to the specified extent.
Nothing ships without final inspection, release note and complete records.
Normas y cumplimiento
Certified systems, and the standards our inspections refer to.
 Certified systemsWelding & NDTMaterials & coating
Resumen solo orientativo: prevalecen la especificación del proyecto, la edición del código adoptada y la autoridad competente.
Quality dossier
What the MDR contains – compiled during fabrication, handed over with the steel.
Section 1
Project quality plan and the agreed inspection and test plan.
Section 2
Approved and released drawings with revisions.
Section 3
EN 10204 certificates with the traceability record.
Section 4
WPS, PQR and welder qualification records.
Section 5
Visual, MT, PT, UT and RT reports.
Section 6
Fit-up, assembly and trial assembly checks.
Section 7
Surface preparation, DFT and adhesion reports.
Sections 8–10
Non-conformances, concessions, release notes and packing lists.
Contents follow the project specification and the agreed ITP; delivered as indexed PDF.
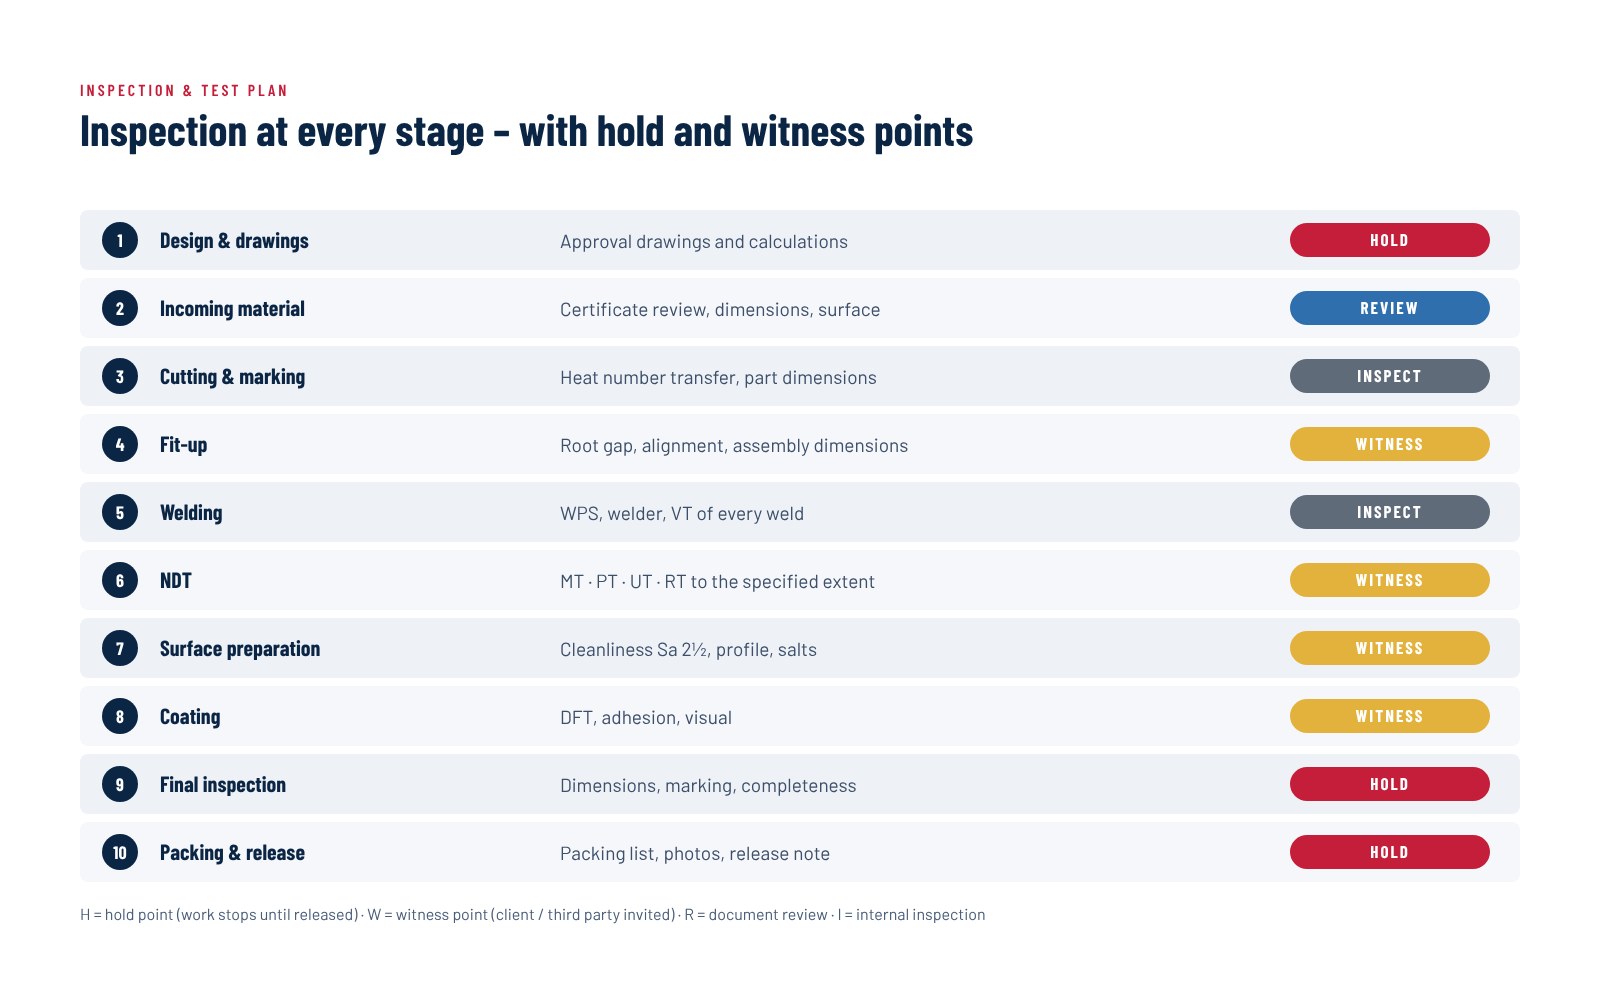
Inspection & test plan
The ITP lists every inspection activity from design to packing, its acceptance criteria and its type: hold points, where work stops until released; witness points, where you or a third-party inspector are invited; and review and internal inspection points. Notifications are sent in advance so inspections never delay production.
Traceability
Every plate and section is received against its mill certificate. When it is cut, the heat number is transferred to each part; when parts are assembled, the piece mark links them to the shop drawing, the welds, the inspection reports and finally the packing list. Ask for any piece on site, and we can show where its steel came from and how it was checked.
Welding & NDT
Welds are made to qualified procedures by qualified welders and visually inspected – every one. Non-destructive testing by MT, PT, UT or RT is carried out by qualified inspectors to the extent and acceptance criteria of the specified code, and every result is recorded against the weld and the piece.
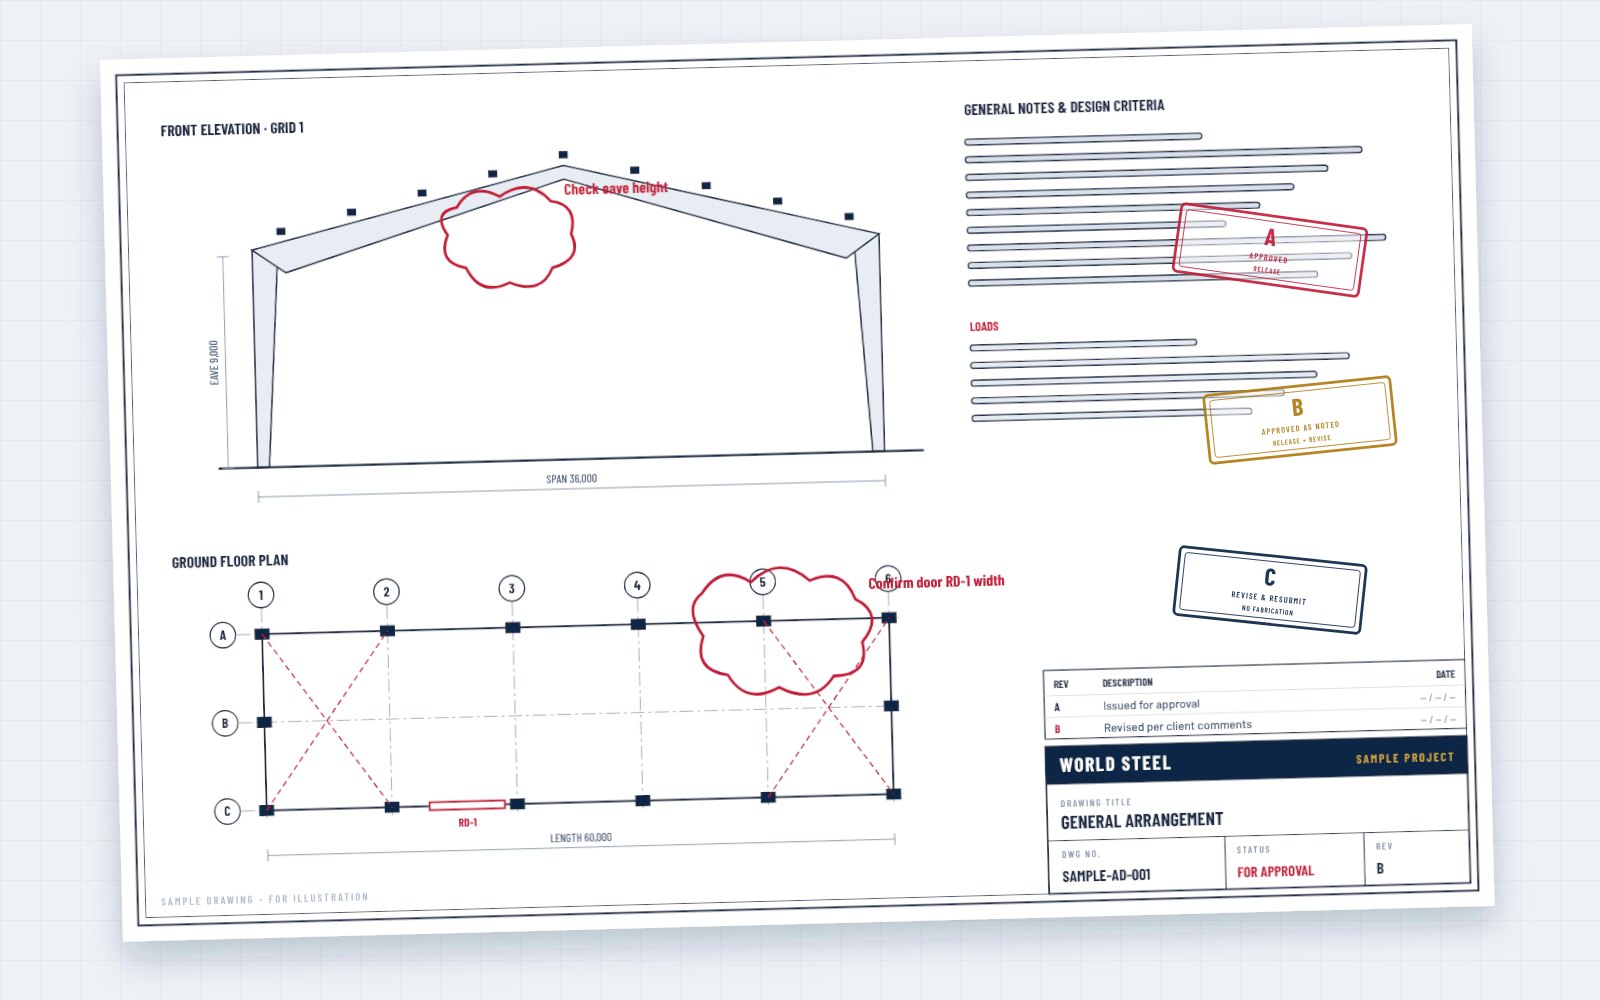
Non-conformance
Any deviation is recorded in a non-conformance report, the piece is quarantined, and the repair or concession is approved before it moves on. Root causes are analysed and corrective actions tracked, and concessions are listed in the dossier – nothing is hidden.
Proceso
Agreed with you before fabrication.
Certificates and material checked.
Heat numbers to every piece.
Qualified welding, VT and NDT.
Checked against drawings and specification.
Final inspection, release and dossier.
Certificación independiente
FAQ
Yes. Witness and hold points are agreed in the ITP and notified in advance; your inspector or a third-party agency is welcome at our factory.
EN 10204 type 3.1 mill certificates for every heat; 3.2 certificates with independent validation can be arranged on request.
Every weld is visually inspected; MT, PT, UT and RT are performed to the extent and acceptance criteria of the specified code or project specification.
The quality plan and ITP, drawing register, material certificates with traceability, welding qualifications, inspection and NDT reports, dimensional and coating records, NCRs and release notes.
Yes – the piece mark links to the heat number, the mill certificate and every inspection record of that piece.
Send us your project specification – we propose the ITP, inspection scope and dossier contents with the quotation.
 EN 1090 EXC3 · CE
 AS/NZS 5131 CC3
 IAS AC472