ENEnglish
 VITiếng Việt
 ZH中文
 KO한국어
 JA日本語
 FRFrançais
 ITItaliano
 PTPortuguês
 ESEspañol
 HEעברית
 ARالعربية

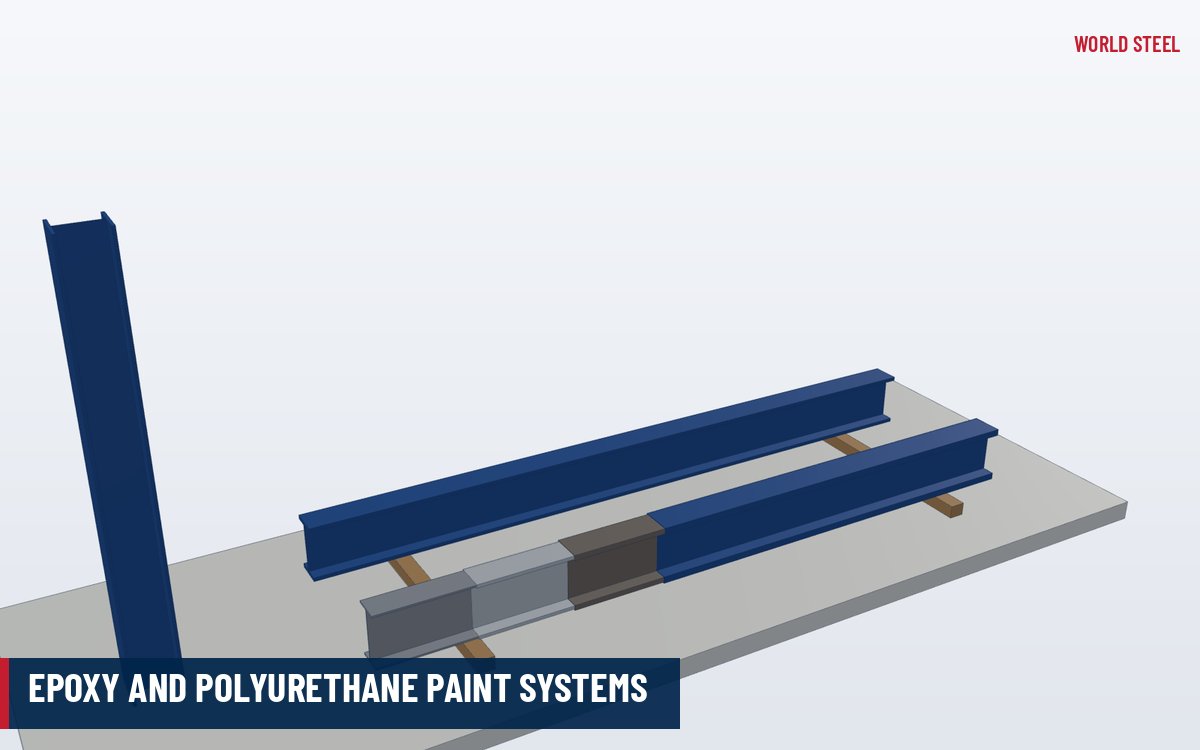
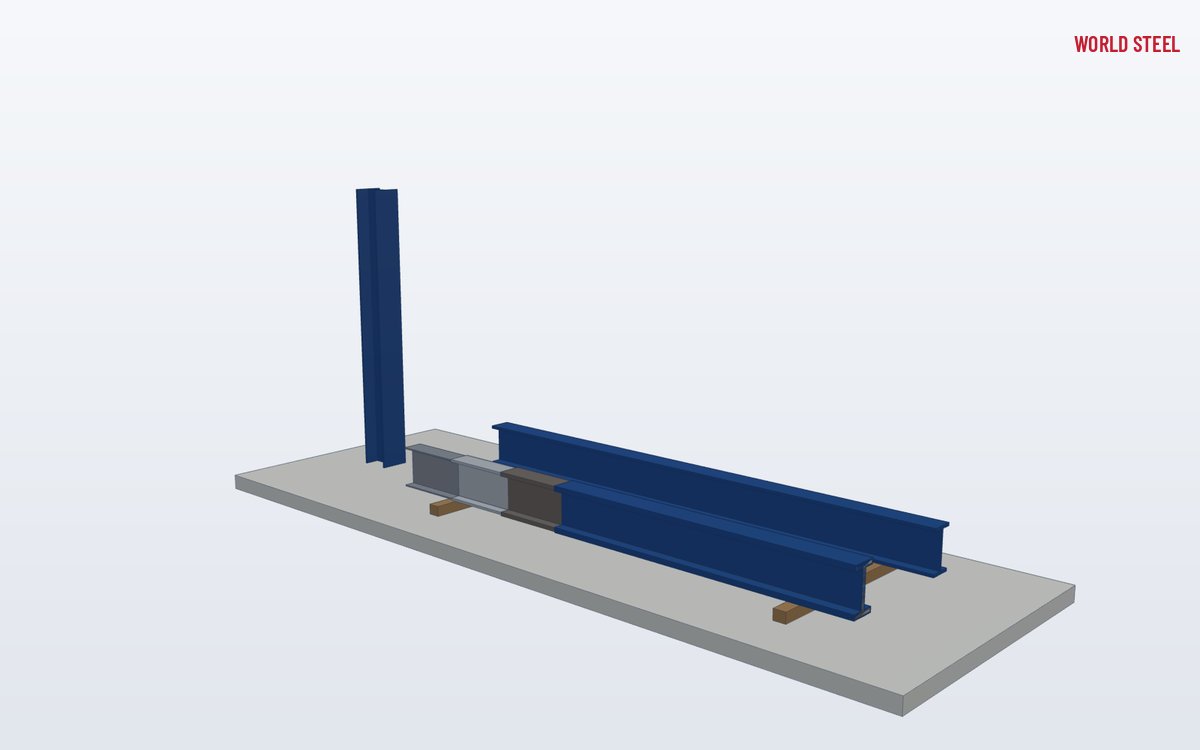
- Zinc-rich epoxy primer for cathodic protection
- Epoxy or epoxy MIO intermediate as a high-build barrier
- Polyurethane topcoat for UV and colour stability
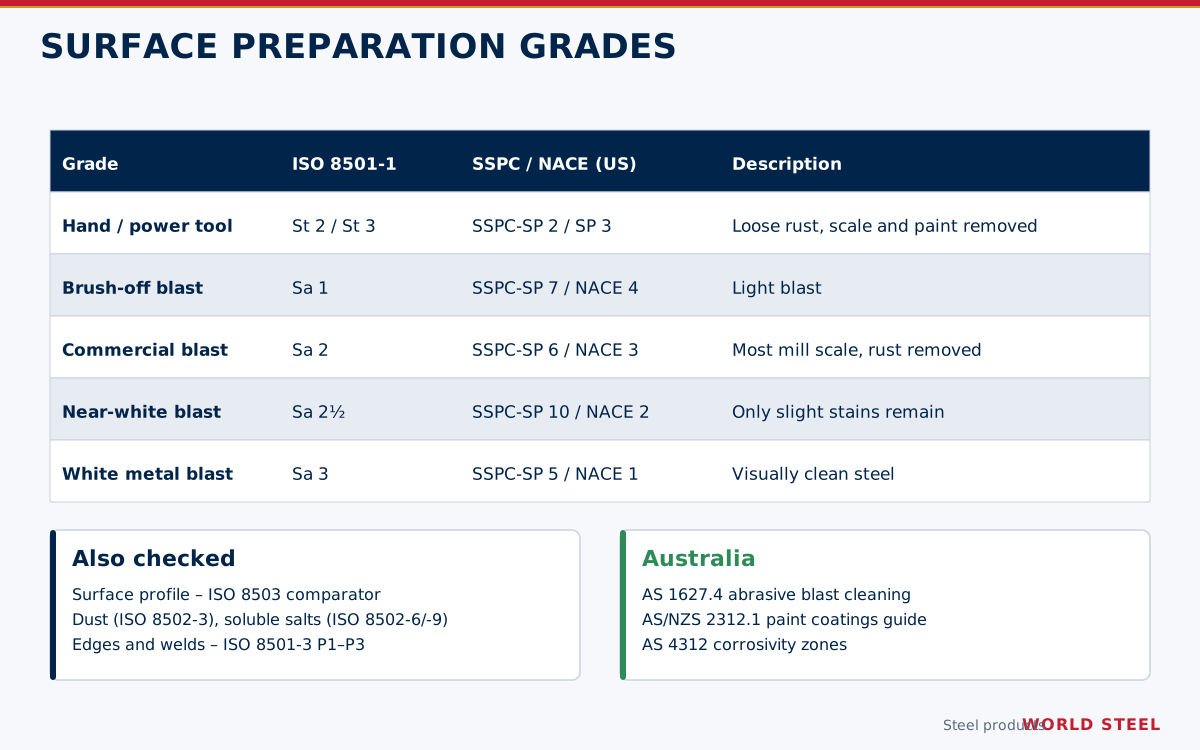
- Blast cleaned to Sa 2½ / SSPC-SP 10 before priming
- Stripe coats on edges, welds and bolt holes
- DFT and adhesion recorded in the coating report
What an epoxy system is
Epoxy paints are two-component coatings: a resin base and a curing agent are mixed before application and cure chemically into a hard, dense film with strong adhesion and good resistance to moisture, chemicals and abrasion. They are the backbone of most industrial and marine paint specifications for structural steel in C3, C4 and C5 environments. Because epoxies chalk and fade in sunlight, an exposed system is finished with a polyurethane (or polysiloxane) topcoat that holds colour and gloss.
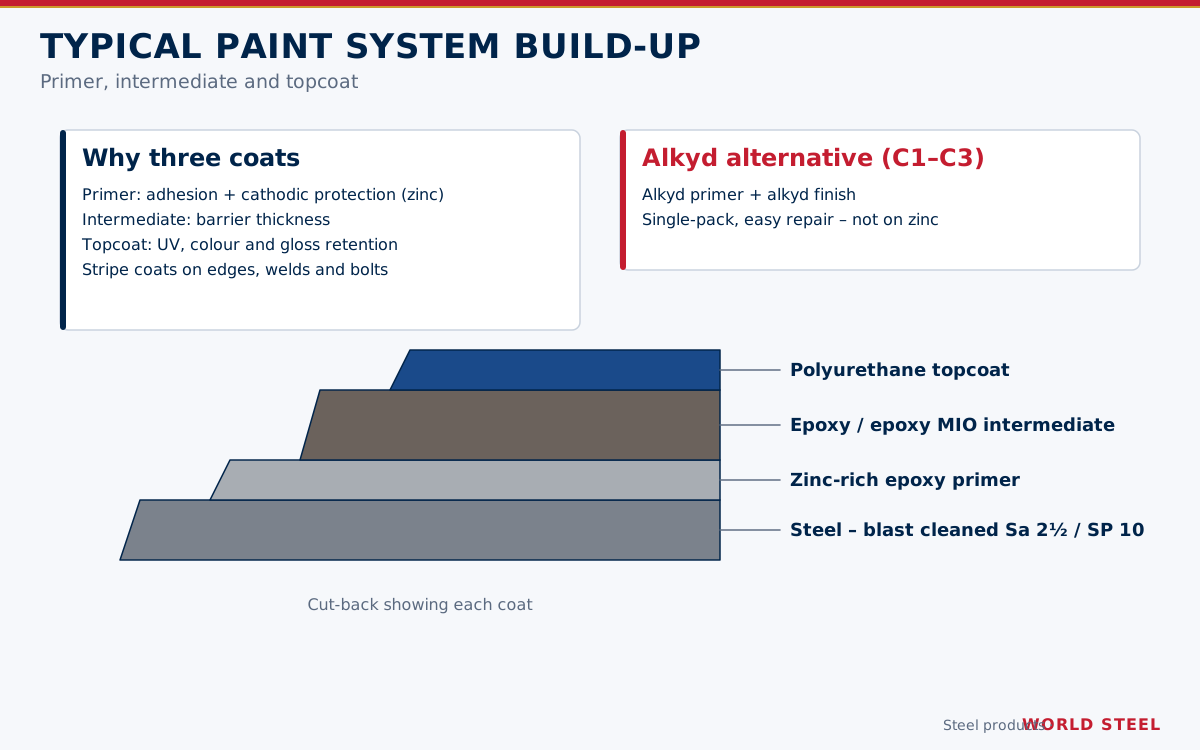
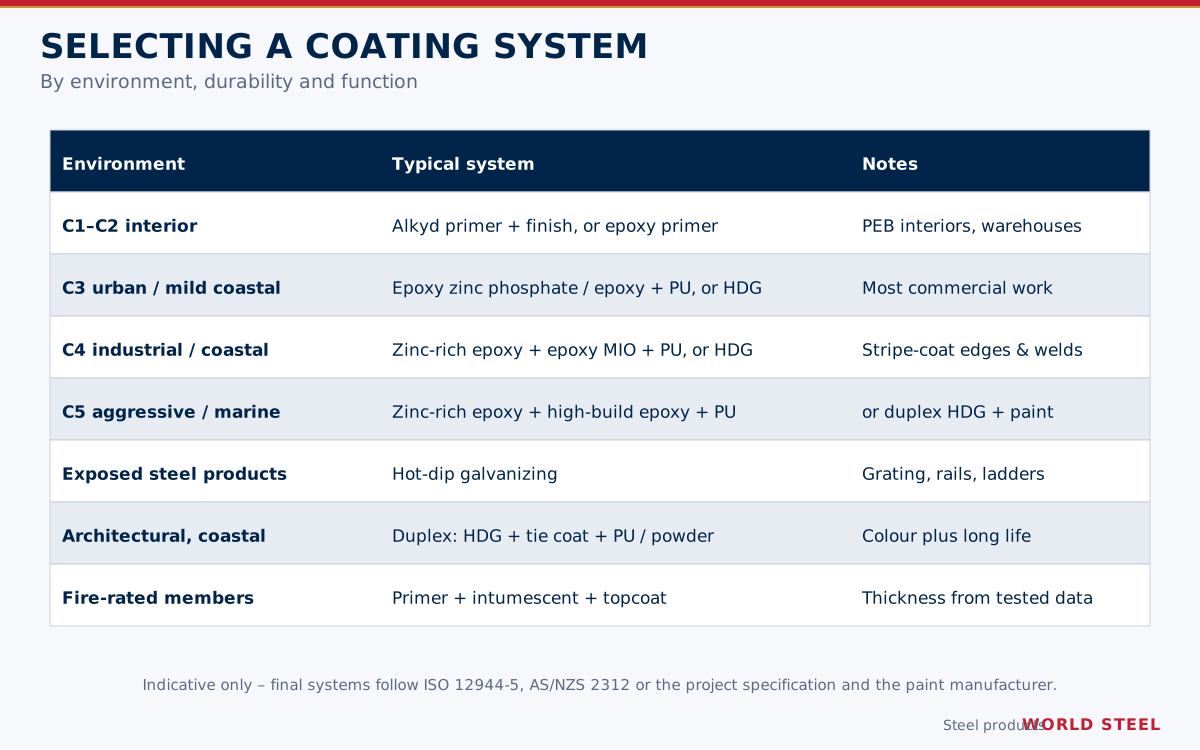
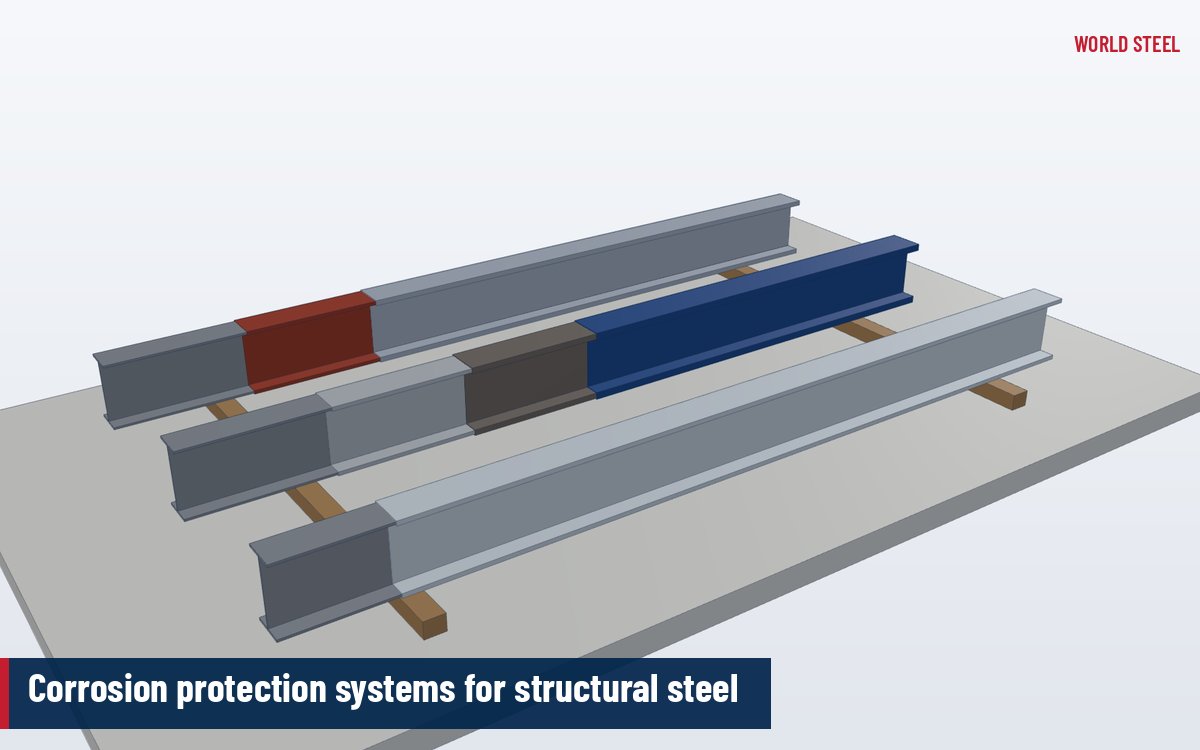
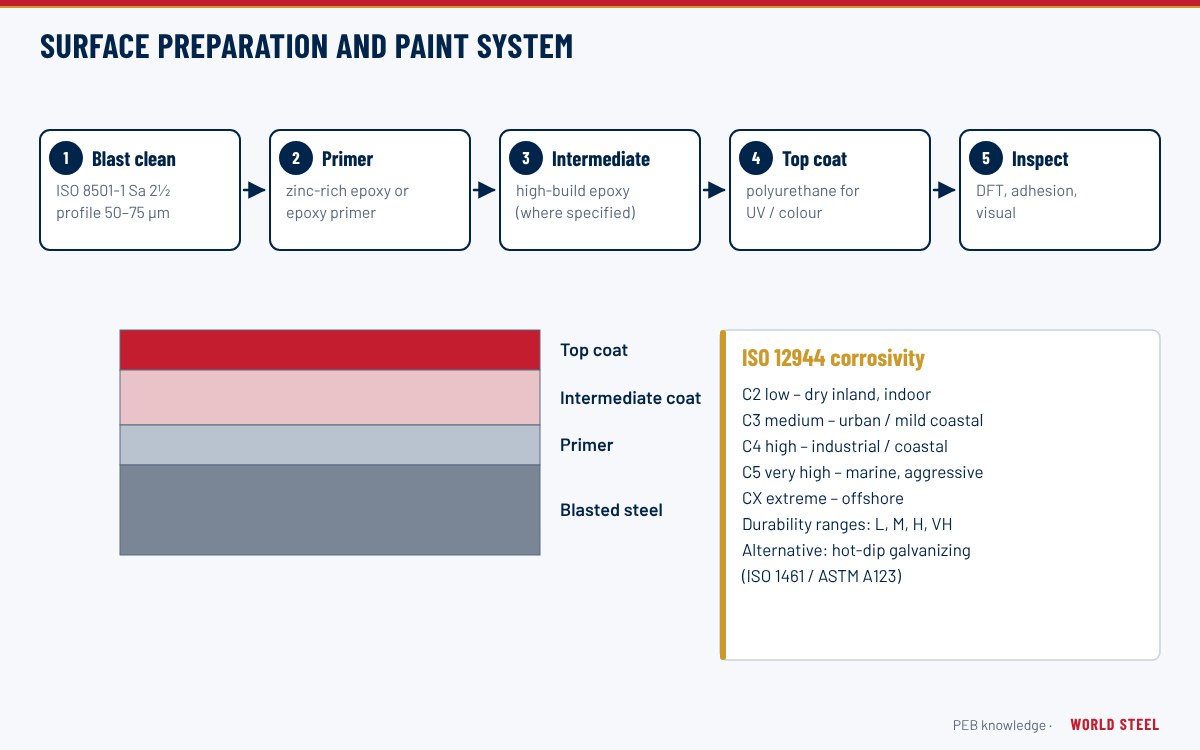
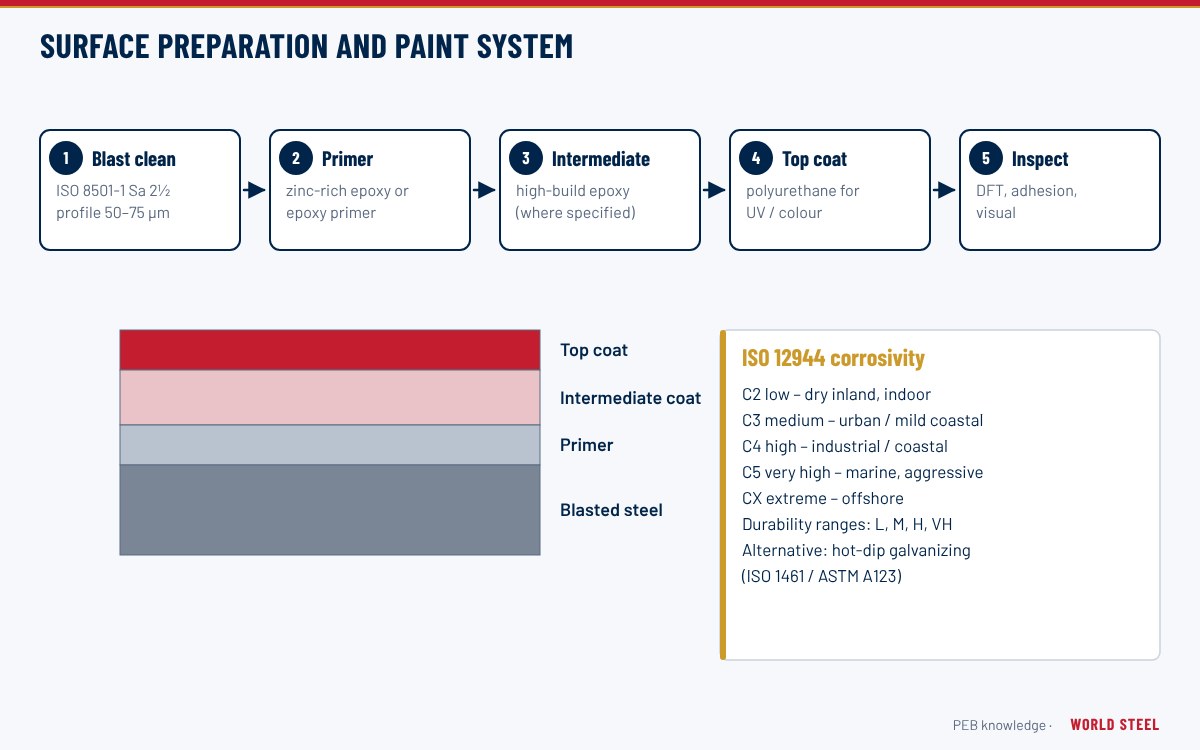
A typical three-coat system has a distinct job for each layer, as shown below. For the choice between epoxy, galvanizing, alkyd and duplex, start with corrosion protection systems; for background on generic paint types see the PEB article on paint and coating systems.
Typical build-ups
The table is qualitative and the thickness ranges are approximate. Three-coat zinc-rich epoxy / epoxy / polyurethane systems with roughly 200–320 µm total nominal DFT are common for C4–C5 with high durability; every project system is confirmed against EN ISO 12944-5 (or AS/NZS 2312.1) and the manufacturer's data sheets.
| Use | Build-up | Approximate total DFT |
|---|---|---|
| Interior, C2–C3, medium durability | Epoxy primer + epoxy finish | Roughly 120–200 µm |
| Exterior, C3–C4, colour exposed | Epoxy or zinc-rich epoxy primer + epoxy intermediate + polyurethane | Roughly 160–260 µm |
| Industrial / coastal, C4–C5, high durability | Zinc-rich epoxy + epoxy MIO intermediate + polyurethane | Roughly 200–320 µm |
| Under intumescent fire protection | Epoxy or zinc-rich epoxy primer approved by the fire coating manufacturer | Per fire coating data sheet |
| Hidden or encased steel, short exposure | Single epoxy primer or shop primer | Per specification |
- Zinc-rich epoxy primer – a high loading of zinc dust gives cathodic protection at scratches and edges; it needs a clean, near-white blasted surface.
- Epoxy or epoxy MIO intermediate – builds film thickness as a barrier; micaceous iron oxide (MIO) flakes lengthen the path for moisture and give a good key for the topcoat.
- Polyurethane topcoat – aliphatic polyurethane gives UV resistance, colour and gloss retention; polysiloxane is an alternative where specified.
Surface preparation and application conditions
Steel is abrasive blast cleaned in the factory to Sa 2½ (ISO 8501-1) / SSPC-SP 10 / NACE No. 2 for zinc-rich and most epoxy primers, with the surface profile set by the data sheet and checked with an ISO 8503 comparator. Welds and edges are prepared to the ISO 8501-3 grade specified (P1–P3), and dust and soluble salts are controlled where the specification requires. Australian work follows AS 1627.4.
Epoxies are sensitive to application conditions. World Steel follows the manufacturer's data sheet for mixing ratio, induction time, pot life, film thickness per coat and minimum and maximum overcoating intervals. Painting proceeds only when the steel temperature is at least 3 °C above the dew point and air temperature and relative humidity are within the data sheet limits; readings are logged. Stripe coats are brushed onto edges, welds, bolt holes and corners before each full coat, because spray films are thinnest there. More detail is in the PEB article on surface preparation and painting.
Inspection and handling
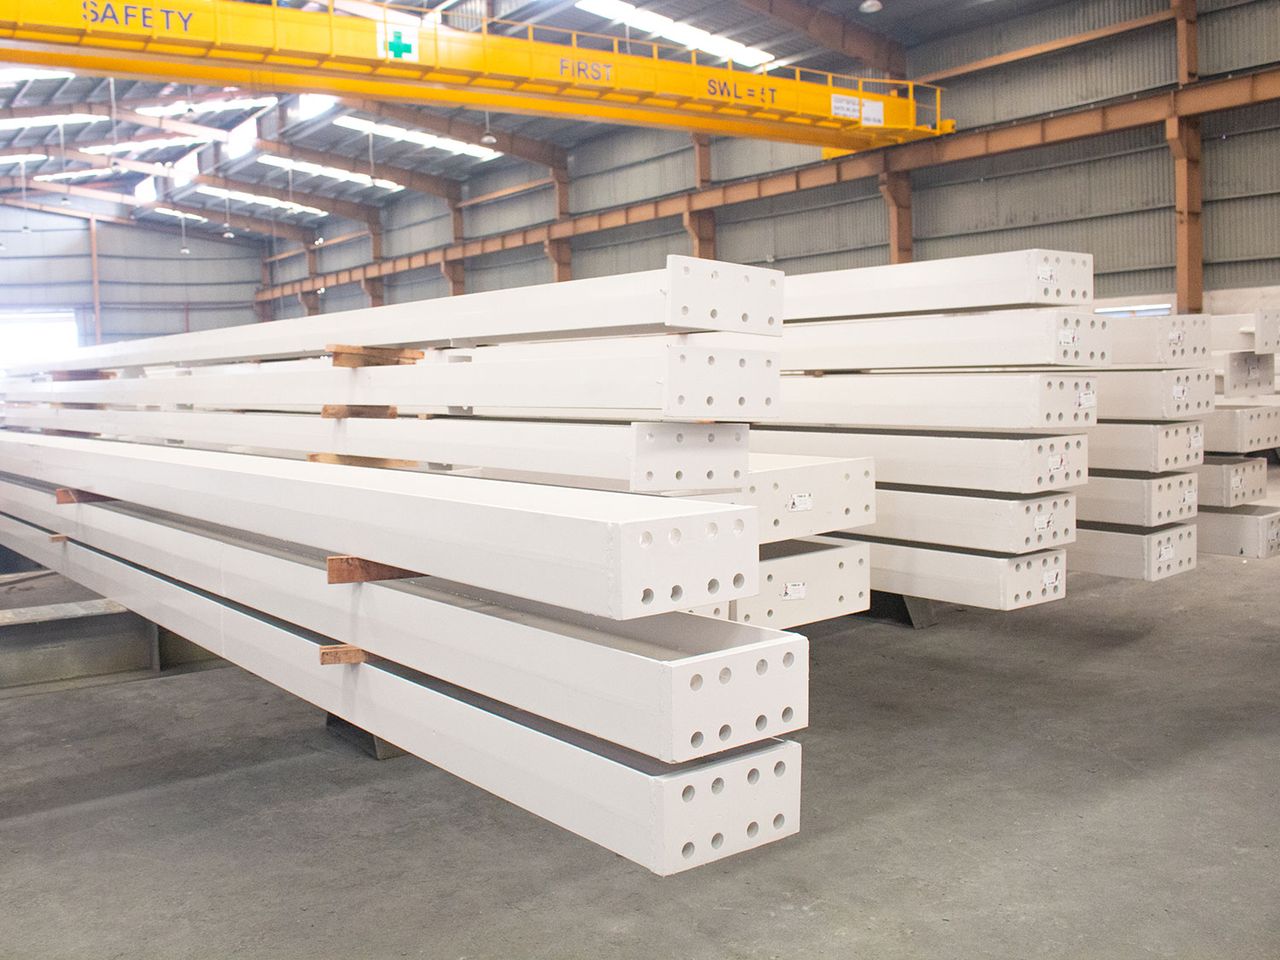
Dry film thickness is measured per coat and in total to ISO 19840 or SSPC-PA 2, depending on the market. Adhesion is checked where specified by pull-off testing (ISO 4624 / ASTM D4541) or cross-cut / tape tests (ISO 2409 / ASTM D3359), and the film is inspected visually for runs, sags, pinholes, dry spray and contamination. Results go into the coating inspection report. Fully cured members are packed with soft slings, timber dunnage and edge protection; contact surfaces of slip-critical bolted joints are masked or coated only with a qualified slip coating as the specification demands.
Epoxy systems are commonly specified on pipe racks, equipment support structures and platforms where the steel must match the plant colour scheme. Systems from manufacturers such as Jotun, Hempel and International Paint are applied at World Steel according to the project specification.
Selecting and specifying
- State the corrosivity category and durability, or the full system with generic types, number of coats and nominal DFT.
- Name the approved manufacturer(s) or ask World Steel to propose an equivalent system with data sheets.
- Give the topcoat colour standard (RAL, AMS-STD-595 or AS 2700) and gloss level.
- Identify faying surfaces, members to receive fire protection and areas to be left uncoated for site welding.
- Agree the touch-up procedure and who supplies touch-up paint for erection damage.
Normas y requisitos por mercado
Códigos con los que World Steel diseña, fabrica y documenta este producto, y los principales requisitos geométricos y de carga en cada mercado.
 Estados Unidos
- SSPC-SP 10 / NACE No. 2Near-white metal blast cleaning
- SSPC-SP 5 / NACE No. 1White metal blast cleaning
- SSPC-PA 2Measurement of dry coating thickness
- ASTM D4541Pull-off strength of coatings
- ASTM D3359Adhesion by tape test
- AMS-STD-595Colours (formerly Federal Standard 595)
- Surface preparation
- SSPC-SP 10 / NACE No. 2 near-white blast for zinc-rich primers (typical)
- DFT acceptance
- Per SSPC-PA 2 and the specified range
 Australia / NZ
- AS/NZS 2312.1Guide to the protection of structural steel – paint coatings
- AS 1627.4Abrasive blast cleaning of steel
- AS 4312Atmospheric corrosivity zones in Australia
- AS/NZS 5131 Certificación WSCFabrication and erection of structural steelwork
- AS 2700Colour standards for general purposes
- System selection
- By corrosivity category and life per AS/NZS 2312.1
- Application conditions
- Steel ≥ 3 °C above dew point (typical, per data sheet)
 Europa
- EN ISO 12944-5Protective paint systems
- EN ISO 12944-7Execution and supervision of paint work
- EN ISO 8501-1Preparation grades Sa 1 – Sa 3
- EN ISO 8503Surface profile of blast-cleaned steel
- EN ISO 19840DFT on rough surfaces
- EN ISO 4624Pull-off test for adhesion
- Surface preparation
- Sa 2½ (EN ISO 8501-1), typical for epoxy systems
- C4–C5 high durability system
- Typically three coats, roughly 200–320 µm NDFT – confirm with EN ISO 12944-5
Resumen solo orientativo: prevalecen la especificación del proyecto, la edición del código adoptada y la autoridad competente.
Acabados
| Acabado | Normas / notas |
|---|---|
| Zinc-rich epoxy / epoxy MIO / polyurethane | SSPC-SP 10 · AS/NZS 2312.1 · EN ISO 12944-5 (C4–C5) |
| Epoxy primer / polyurethane | SSPC-SP 10 · AS/NZS 2312.1 · EN ISO 12944-5 (C3–C4) |
| Epoxy primer for intumescent | Per fire coating manufacturer approval in all markets |
Preguntas frecuentes
Why does an exterior epoxy system need a polyurethane topcoat?
Epoxies chalk and lose colour in sunlight. An aliphatic polyurethane (or polysiloxane) topcoat protects the epoxy layers from UV and keeps the colour and gloss stable.
How thick is a typical C5 system?
Three-coat zinc-rich epoxy / epoxy / polyurethane systems of roughly 200–320 µm total are common for C4–C5 with high durability. The exact system must be confirmed with ISO 12944-5 and the manufacturer's data sheets.
Can you paint in high humidity?
Only within the data sheet limits. World Steel checks and logs air temperature, relative humidity, steel temperature and dew point, and paints only when the steel is at least 3 °C above the dew point.
Which paint manufacturers can you use?
Systems from international manufacturers such as Jotun, Hempel, AkzoNobel (International Paint) and Carboline, and regional manufacturers, are applied according to the project specification.
 Qatar
 AS/NZS 5131 CC3
 EN 1090 EXC3 · CE