ENEnglish
 VITiếng Việt
 ZH中文
 KO한국어
 JA日本語
 FRFrançais
 ITItaliano
 PTPortuguês
 ESEspañol
 HEעברית
 ARالعربية

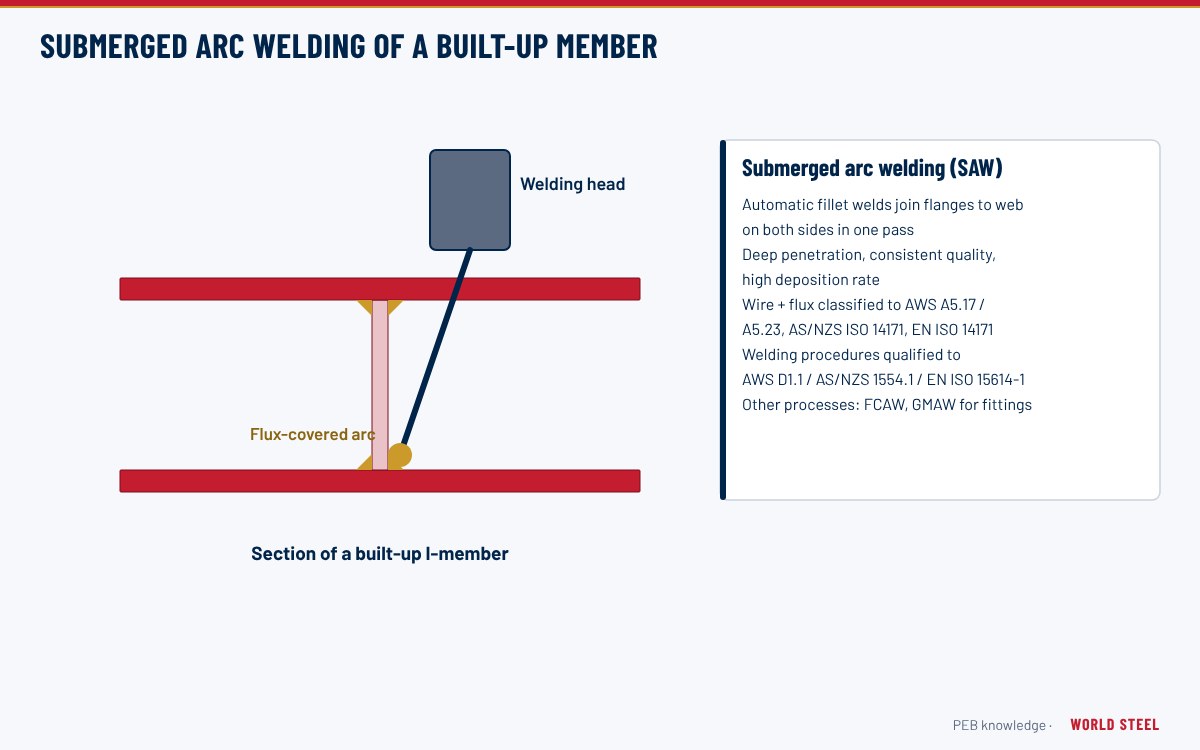
Welding in PEB fabrication
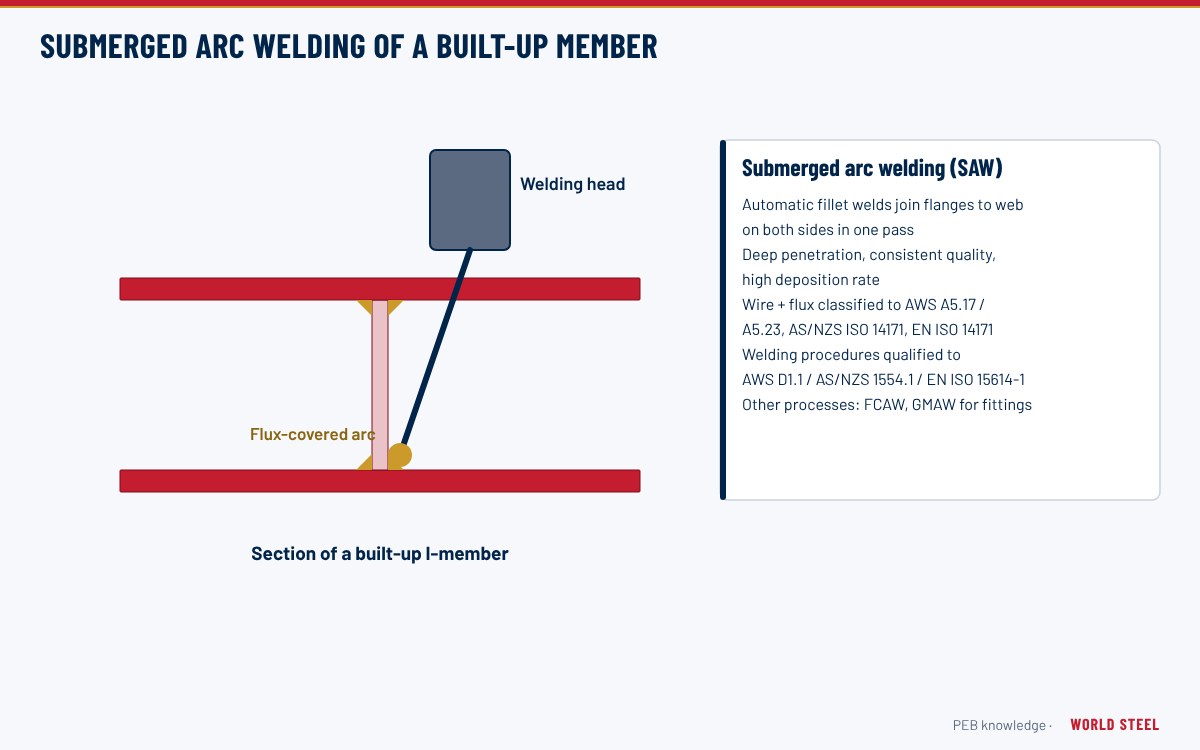
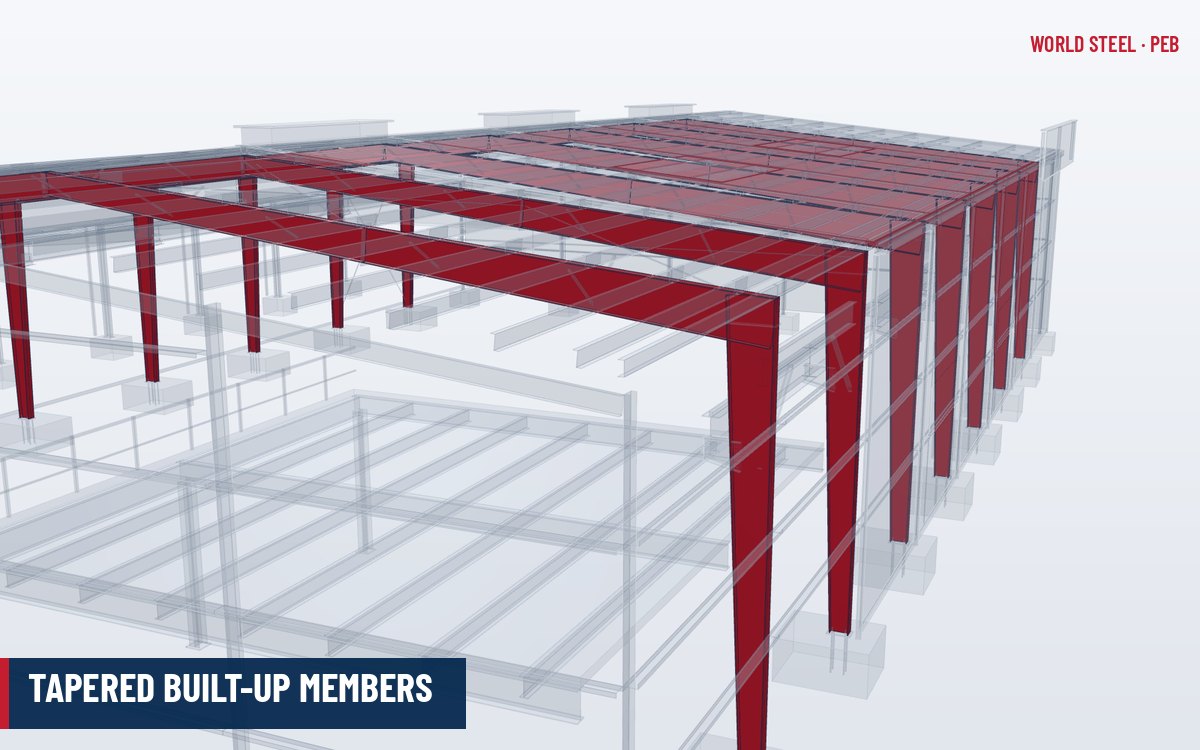
Every primary member of a pre-engineered building is a welded product. Long web-to-flange fillet welds of tapered built-up members are made by automatic machines; end plates, stiffeners, clips and base plates are welded manually or semi-automatically. Weld quality therefore controls structural reliability. The choice of process, consumable classification matched to the base metal, and qualified procedures and welders are the three pillars that codes such as AWS D1.1, AS/NZS 1554.1 and EN 1090-2 with EN ISO 3834 regulate.
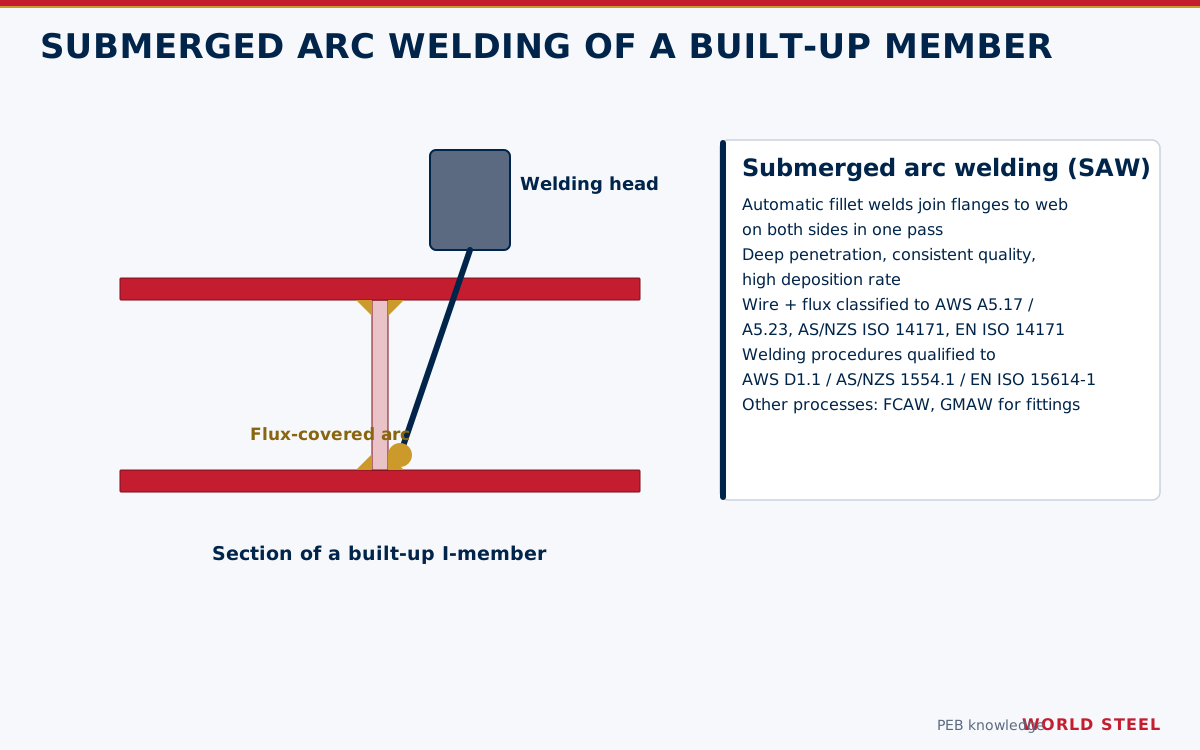
Welding processes used
| Process | Typical use | Characteristics |
|---|---|---|
| Submerged arc welding (SAW, ISO 4063 process 121) | Web-to-flange fillet welds on automatic lines; long butt welds in plate | High deposition, deep penetration, excellent appearance; flat or horizontal position only |
| Flux-cored arc welding (FCAW, 136 gas-shielded) | End plates, stiffeners, base plates, all-position work | High productivity, good positional capability, slag cover |
| Gas metal arc welding (GMAW / MAG, 135) | Clips, light connections, secondary items, robotic welding | Clean, fast, low spatter with mixed gas; sensitive to drafts |
| Shielded metal arc welding (SMAW, 111) | Repairs, site work | Versatile, low productivity |
Consumable classifications
Consumables are classified by standards that define strength, toughness and chemistry of the deposited weld metal. Matching consumables for 345–355 MPa steels typically have about 490 MPa (70 ksi) minimum tensile strength.
| Process | AWS (US / Canada) | ISO / AS/NZS / EN |
|---|---|---|
| SAW | AWS A5.17, e.g. F7A2-EM12K (or A5.23 for low-alloy) | ISO 14171-A, e.g. S 38 2 AB S2 / AS/NZS ISO 14171 / EN ISO 14171 |
| FCAW | AWS A5.20 E71T-1C / -1M (A5.36 under the newer combined system) | ISO 17632, e.g. T 46 2 P C1 / AS/NZS ISO 17632 / EN ISO 17632 |
| GMAW | AWS A5.18 ER70S-6 | ISO 14341, e.g. G 42 3 M21 3Si1 / AS/NZS ISO 14341 / EN ISO 14341 |
| SMAW | AWS A5.1 E7018 | ISO 2560, e.g. E 42 3 B / AS/NZS ISO 2560 / EN ISO 2560 |
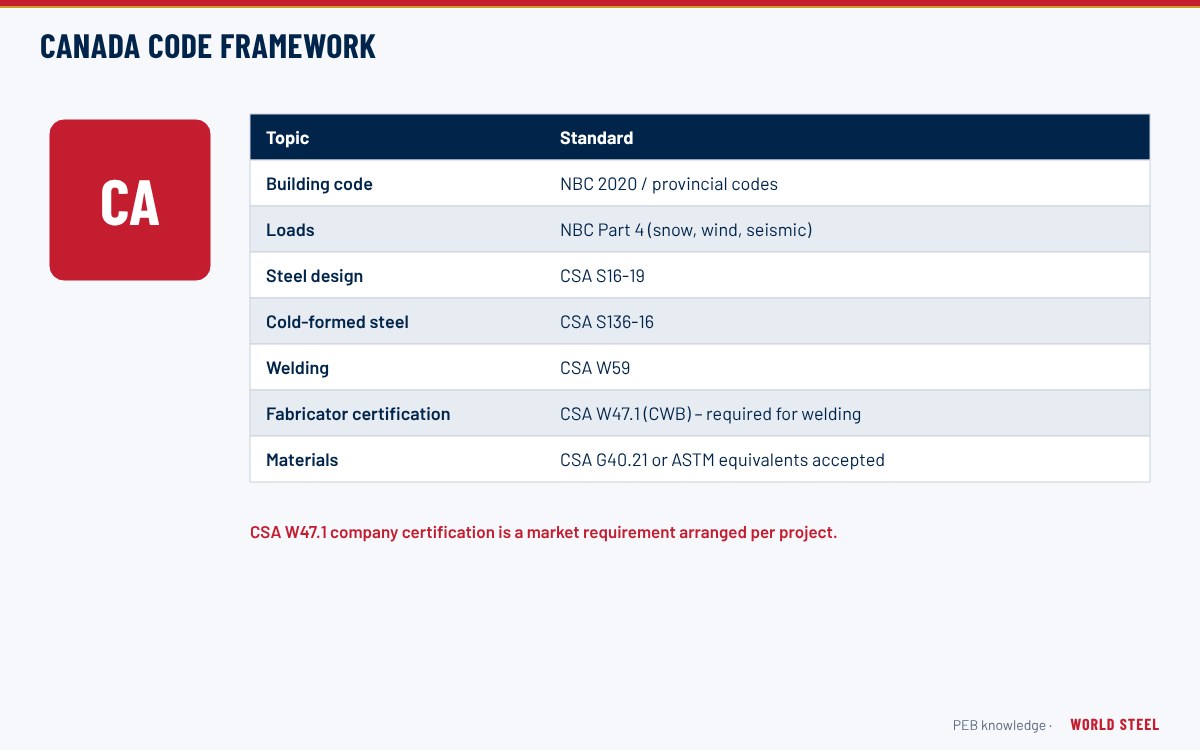
In Canada, consumables are certified to CSA W48 and welding companies are certified to CSA W47.1; in Australia, AS/NZS 1554.1 references the AS/NZS ISO consumable standards. Low-hydrogen consumables (H8 or better) are recommended for thicker plates, restrained joints and higher-strength steels. Consumables must be stored and, where required, baked per manufacturer guidance.
Shielding gases, fluxes, hydrogen control and preheat
A matching wire or electrode is only part of the consumable system. Gas, flux and storage conditions change weld metal properties as much as the filler itself.
| Item | Typical practice | Reference |
|---|---|---|
| Shielding gas | CO₂ (C1) or argon-CO₂ mixtures such as M21 for FCAW and GMAW; gas type must match the consumable classification | ISO 14175; AWS A5.32 |
| SAW flux | Agglomerated or fused flux matched to the wire; recycled flux sieved and kept dry | AWS A5.17 / ISO 14174 |
| Diffusible hydrogen | Consumables designated H8 or H4 for thick or restrained joints | AWS A4.3 / ISO 3690 |
| Electrode storage | Low-hydrogen electrodes kept in heated ovens after opening and rebaked per manufacturer data | AWS D1.1 storage clauses; manufacturer guidance |
| Preheat | Minimum temperature by steel grade, carbon equivalent, thickness and hydrogen level | AWS D1.1 prequalified preheat table; AS/NZS 1554.1 preheat provisions; EN 1011-2 |
For seismic force-resisting systems designed to AISC 341-22, demand-critical welds require filler metals with specified notch toughness and testing per AWS D1.8; in PEB this mainly affects end-plate and base connections of moment frames in high-seismic regions. In thin PEB plates (webs of about 4–8 mm), preheat is rarely required for 350 MPa steel, but thick base plates, crane girder flanges and cold conditions can trigger it.
Procedures, welders and inspection
- Procedures: AWS D1.1 allows prequalified WPSs within defined limits; others are qualified by PQR testing. AS/NZS 1554.1 has prequalified procedures; EN 1090-2 requires WPS qualified to EN ISO 15614-1 or equivalent routes depending on execution class.
- Welders and operators: qualified to AWS D1.1 Clause 6, AS/NZS 2980 / ISO 9606-1, or ISO 14732 for operators of mechanised equipment.
- Quality management: EN ISO 3834-2 (comprehensive quality requirements) is required for EXC3 work in Europe.
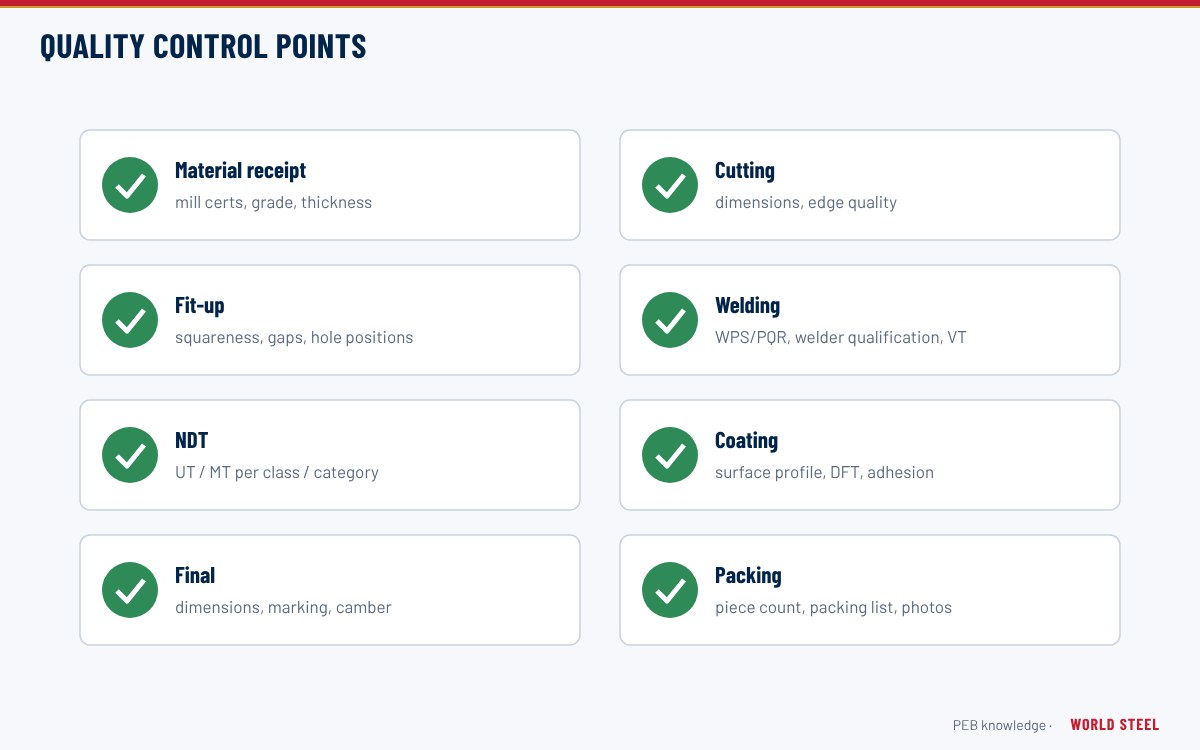
- Inspection: visual inspection of all welds; ultrasonic (UT) or magnetic particle (MT) testing at frequencies set by the code, execution class or category (e.g. SP or GP in AS/NZS 1554.1).
- Distortion control: sequencing and fixturing on automatic lines keep tapered members straight within tolerance.
Welding at WSC
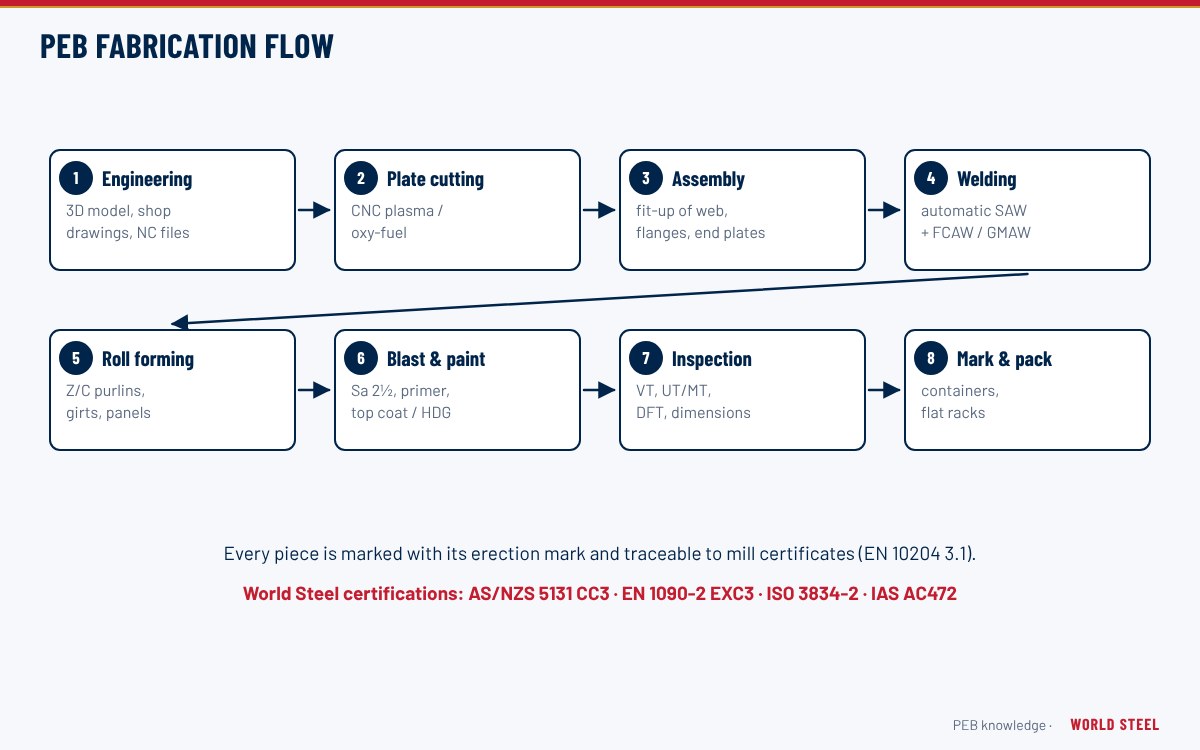
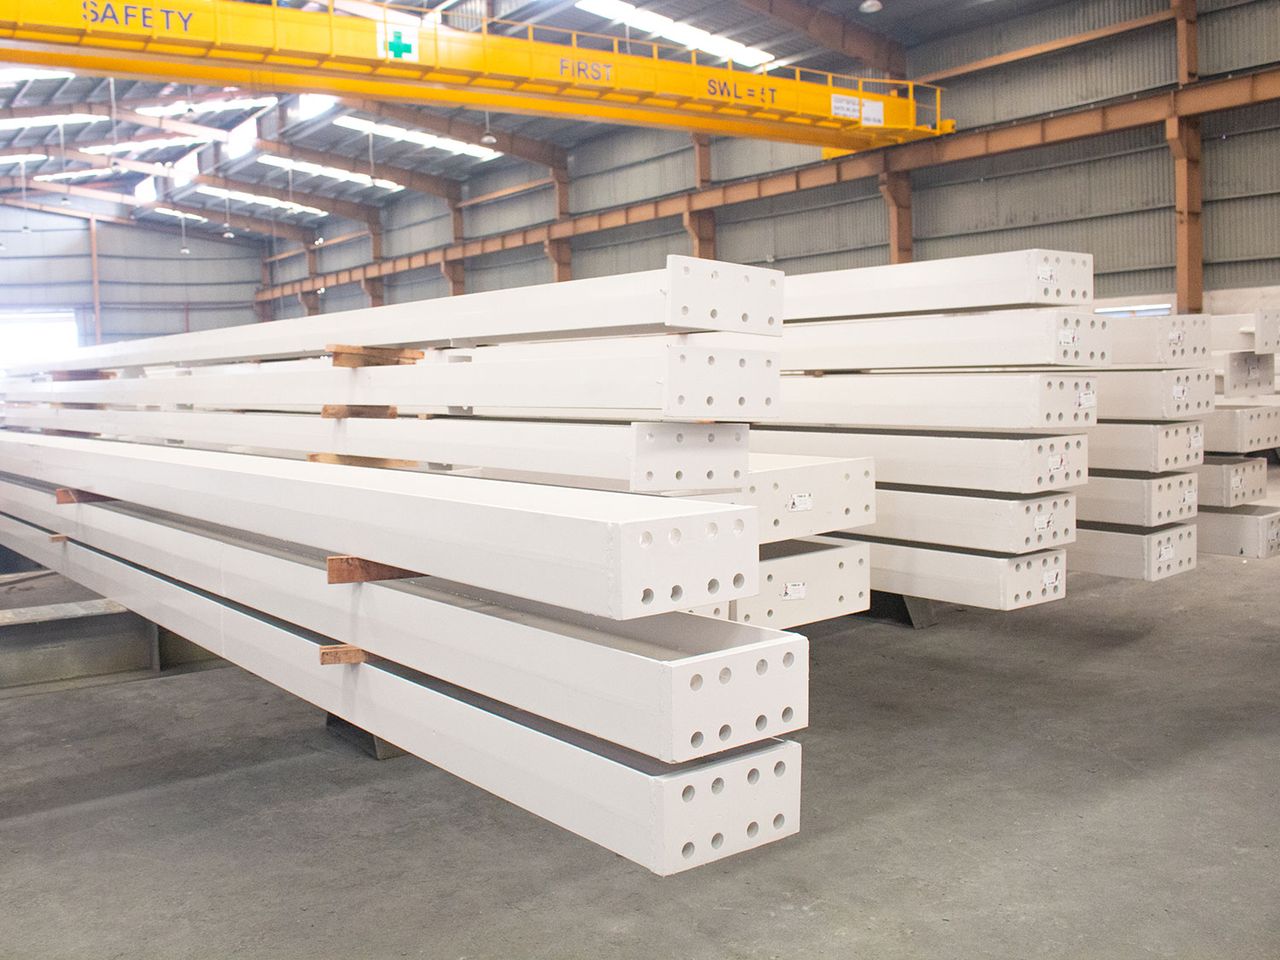
World Steel welds built-up members on automatic SAW lines and uses FCAW and GMAW for fittings, under procedures and welder qualifications to the welding code specified for each project, within an ISO 3834-2 certified welding quality system and EN 1090-2 EXC3 and AS/NZS 5131 CC3 certifications. Consumables are sourced from established international and regional producers and matched to the steel grade of each project. See automatic welding of built-up members, quality control and inspection, and WSC's manufacturing capability.
Normas por región
| Región | Norma | Alcance |
|---|---|---|
 United States |
AWS D1.1 / D1.3 | Structural welding code – steel; sheet steel |
| United States |
AWS A5.17 / A5.20 / A5.18 / A5.36 | Filler metal specifications |
 Canada |
CSA W59 / W47.1 / W48 | Welded steel construction; company certification; consumables |
 Australia / NZ |
AS/NZS 1554.1 | Structural steel welding – welding of steel structures |
| Australia / NZ |
AS/NZS ISO 14341 / 17632 / 14171 | Wire, tubular cored and SAW consumables |
 Europe |
EN 1090-2 / EN ISO 3834-2 | Execution of steel structures; welding quality requirements |
| International | ISO 15614-1 / ISO 9606-1 | Procedure and welder qualification |
Preguntas frecuentes
Why is submerged arc welding used for PEB members?
SAW deposits weld metal quickly with deep penetration and consistent quality, ideal for the long web-to-flange welds of built-up members produced on automatic lines.
What does E71T-1C mean?
An AWS A5.20 flux-cored electrode with 70 ksi minimum tensile strength, usable in all positions (1), gas-shielded with CO2 (C). It is a common FCAW wire for structural steel.
Does a Canadian project need CSA W47.1?
Canadian building codes generally require fabricators of welded structural steel to be certified to CSA W47.1 by the CWB. This must be arranged and confirmed for each Canadian project.