 ENEnglish
 VITiếng Việt
 ZH中文
 KO한국어
 JA日本語
 FRFrançais
 ITItaliano
 PTPortuguês
 ESEspañol
 HEעברית
 ARالعربية

What AS/NZS 5131 covers – and what it does not
AS/NZS 5131:2016 (incorporating Amendment 1, 2020) sets minimum requirements for constructing structural steelwork: fabrication, surface preparation, painting and galvanizing, erection and modification. Under Clause 1.1 it applies to complete structures, individual members and prefabricated components, made from hot-rolled and welded sections and plate (design yield stress up to 690 MPa), cold-formed hollow sections to AS/NZS 1163, weathering steel, composite steel–concrete members and cold-formed purlins, girts and decking. The design basis is AS 4100, AS 5100.6, AS 2327.1, AS/NZS 4600 or NZS 3404 as relevant.
The Standard is deliberately broad: buildings, general structures, crane runway girders, monorails and road, rail and pedestrian bridges are all in scope, including members subject to seismic actions or fatigue. Clause 1.2 lists the structures and elements included – from conveyor and bin supports, towers, stairs and walkways to base plates, holding-down bolts, bracing, connection plates, fasteners, shear studs and handrails – provided they are shown and sized on the structural drawings and carry design loads.
Clause 1.3 excludes, among other things, stainless steel, castings and forgings, wire and cable elements, hot-driven rivets, proprietary bearings and expansion joints, crane rails, roof and wall sheeting, light-gauge framing (other than AS/NZS 1163 hollow sections), formwork, scaffolding, storage racking and steel-framed housing. Those items need their own specification. Provisions on weld and bolt inspection that apply only in New Zealand sit in Appendix I.
The construction category concept (Clause 4.1.2)
Many requirements in the Standard are graded by construction category. Four categories – CC1, CC2, CC3 and CC4 – are defined, and strictness increases from CC1 to CC4. Three rules matter in practice:
- The designer nominates the category in the construction specification. If the specification is silent, CC2 applies by default – a common gap when overseas fabrication is procured from a generic specification.
- A CC can apply to the whole structure, part of it or specific details. One project can carry several categories, provided every part is categorised.
- CC4 is not fully defined. It is CC3 plus additional requirements set at project level or by an owner or agency, for unusual or special structures.
The category is one of the items the construction specification must state under Clause 4.1.1; the specification itself is covered in the next chapter, construction specification and documentation.
The three inputs in Appendix C
Appendix C (informative) explains that choosing a CC is a risk-based decision aligned with the reliability philosophy of AS/NZS 1170. Quality assurance during fabrication and erection is treated as one of the measures that delivers the reliability assumed in design. The designer combines three inputs (Paragraph C3):
| Input | What it reflects | Lower class | Higher class |
|---|---|---|---|
| Importance level (IL1–IL4) | Risk to life and consequences of failure, from the NCC in Australia or AS/NZS 1170.0 Section 3 | IL1 – low-consequence structures | IL4 – post-disaster and essential facilities |
| Service category (Table C1) | Uncertainty in actions that could expose flaws in service | SC1 – predominantly quasi-static loading, low seismic demand or fatigue not requiring assessment | SC2 – members needing fatigue assessment, or medium–high seismic demand (EDC III in Australia) |
| Fabrication category (Table C2) | Complexity of fabrication | FC1 – non-welded work, or welded work in steel up to Grade 450 | FC2 – welded steel above Grade 450, structurally essential site welds, heat-treated components, profiled CHS truss ends |
The service category is also used later to set the recommended extent of weld NDE (Clause 12.6.10), so it should be stated in the specification even when the CC is already given.
Reading the risk matrix
Paragraph C4 combines the three inputs in a matrix – Table C3 for Australia and Table C4 for New Zealand. Without reproducing the tables, the pattern in the Australian matrix is:
- CC1 appears only for the lowest combination: importance level 1, quasi-static service and simple fabrication.
- CC2 covers most ordinary IL1–IL2 structures under quasi-static loading.
- Any SC2 combination is at least CC3 – fatigue-loaded or seismically demanding steelwork moves up regardless of importance level.
- For importance level 3 with SC1 and FC1, the result is CC2 or CC3 by engineering judgement, based on how simple fabrication and erection are.
- Importance level 4 is CC3, and CC4 appears only where IL4, SC2 and FC2 coincide.
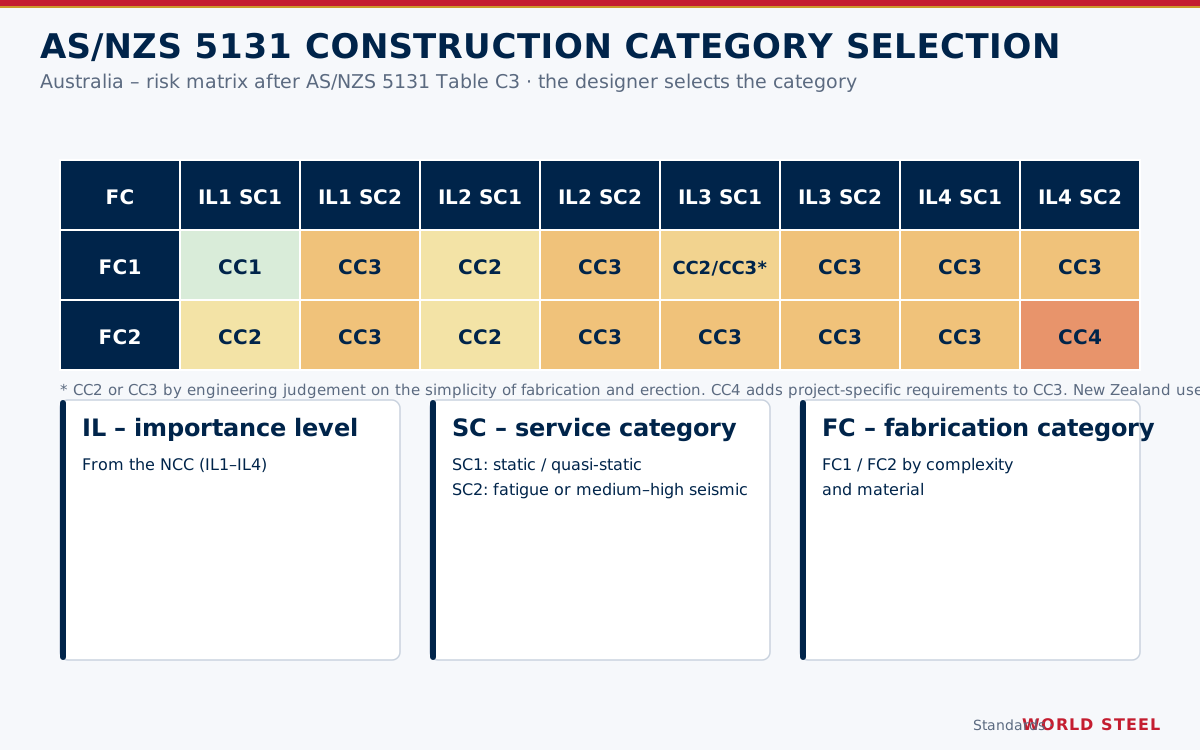
The New Zealand matrix groups IL3 and IL4 together (all CC3), treats IL1–IL2 differently, places IL5 outside its scope and assigns road and rail bridges with fracture-critical components to CC4. Table C3 notes that the decision rests with the designer, taking account of national provisions, industry guidance and WHS requirements. Refer to the current edition of AS/NZS 5131 for the full matrices.
The CC is a design decision, not a fabricator's choice. World Steel works to the category stated in the construction specification and raises an RFI when it is missing or appears inconsistent with the structure.
Where CC3 typically applies
Final selection always depends on the project, but the inputs above tend to put the following steelwork at CC3:
- Crane runway girders and their supports, where fatigue assessment is required, and structures excited by machinery, crowds or wind.
- Road, rail and pedestrian bridges subject to fatigue (with fracture-critical NZ bridges going to CC4).
- Structures in earthquake design category III in Australia, or seismic system categories 1 and 2 in New Zealand – see seismic steel structures.
- Importance level 4 facilities, and IL3 buildings where the designer judges the fabrication complex enough.
- Mining, processing and conveyor structures with vibrating plant, which usually fall into SC2.
A typical IL2 warehouse or portal frame in Grade 300/350 steel with quasi-static loading would usually be CC2 – but a client may still choose a CC3-certified fabricator to cover mixed-category projects.
What actually changes between categories
Appendix B, Paragraph B4 lists only the requirements that differ by category; the full requirements remain in the body of the Standard. Selected differences relevant to a fabricator:
| Topic (clause) | CC1 | CC2 | CC3 / CC4 |
|---|---|---|---|
| Quality plan (4.5.2) | No particular requirement | If the specification requires it | Required |
| Welding quality system (7.1.1) | AS/NZS 1554 or ISO 3834-4 recommended | ISO 3834-3 recommended | ISO 3834-2 comprehensive recommended |
| Welder qualification (7.4.2) | To AS/NZS 1554 | To AS/NZS 1554 | To AS/NZS 2980 or ISO 9606-1 |
| Component identification and traceability, Australia (6.2) | Basic | Partial | Full |
| Holing (6.7.1) | Punching permitted | Punching permitted | Punching followed by reaming |
| Functional tolerance class (12.1) | Class 1 recommended | Class 1 recommended | Class 2 recommended |
| Single-sided welds with permanent backing (7.5.9.2) | No particular requirement | No particular requirement | Backing made continuous |
Documented ITPs for preparation, assembly, bolting and erection are required from CC2 upwards, and NDE extent follows Table 13.6.2.2. These topics are expanded in the welding and inspection and testing chapters.
Why fabricator certification at CC3 matters
Because CC3 adds the comprehensive welding quality system, higher welder qualification, full traceability and a project quality plan, a fabricator certified at CC3 has demonstrated the systems needed for CC2 work as well. World Steel holds AS/NZS 5131 CC3 product certification (BSI Group ANZ Benchmark, certificate BMP 827566, JAS-ANZ accredited, valid to 31 July 2030) for its Hai Son Industrial Park facility in Tay Ninh, supported by ISO 3834-2 certification. Certification shows capability; compliance on each project is still demonstrated through that project's ITP, records and inspections against its own construction specification.
평가자 체크리스트
AS/NZS 5131의 이 부분과 관련하여 엔지니어, 시공사 또는 감사자가 CC3 제작사에서 확인해야 할 사항과 요청해야 할 증빙.
| 조항 · CC | 확인 사항 | 증빙 |
|---|---|---|
| 4.1.2 CC1–CC4 | The construction category for each part of the works is identified from the specification, and the CC2 default is flagged where none is stated. | Contract review record, construction specification extract |
| 1.3 CC1–CC4 | Excluded items (e.g. stainless steel, castings, crane rails) are identified and dealt with under their own specification. | Scope review, RFI log |
| Appendix C CC3 | Mixed-category projects have each element or detail mapped to its CC on drawings or in the model. | Designer's CC nomination, RFI responses |
| 4.5.2 CC3–CC4 | A project-specific quality plan is prepared before fabrication starts. | Project quality plan |
| 7.1.1 CC3–CC4 | Welding is managed under a comprehensive welding quality system. | ISO 3834-2 certificate, welding coordination records |
| 7.4.2 CC3–CC4 | Welders on CC3 work hold the higher qualification level. | Welder qualification certificates to AS/NZS 2980 or ISO 9606-1 |
| 6.2 CC3–CC4 | Full identification and traceability of components is maintained through fabrication. | Marking procedure, material register, piece-mark records |
| 6.7.1 CC3–CC4 | Holes are drilled, or punched and then reamed, as required at CC3. | Holing procedure, CNC drilling records |
| 12.1 CC3–CC4 | Functional tolerances are checked to the class specified (Class 2 is recommended at CC3). | Dimensional inspection records |
| Certification CC3 | The fabricator's certificate covers CC3, the actual fabrication site and is current. | Product certificate, scope and expiry date |