ENEnglish
 VITiếng Việt
 ZH中文
 KO한국어
 JA日本語
 FRFrançais
 ITItaliano
 PTPortuguês
 ESEspañol
 HEעברית
 ARالعربية

- Systems selected by ISO 12944-2 corrosivity category C1–CX
- Durability ranges L, M, H and VH to ISO 12944-1
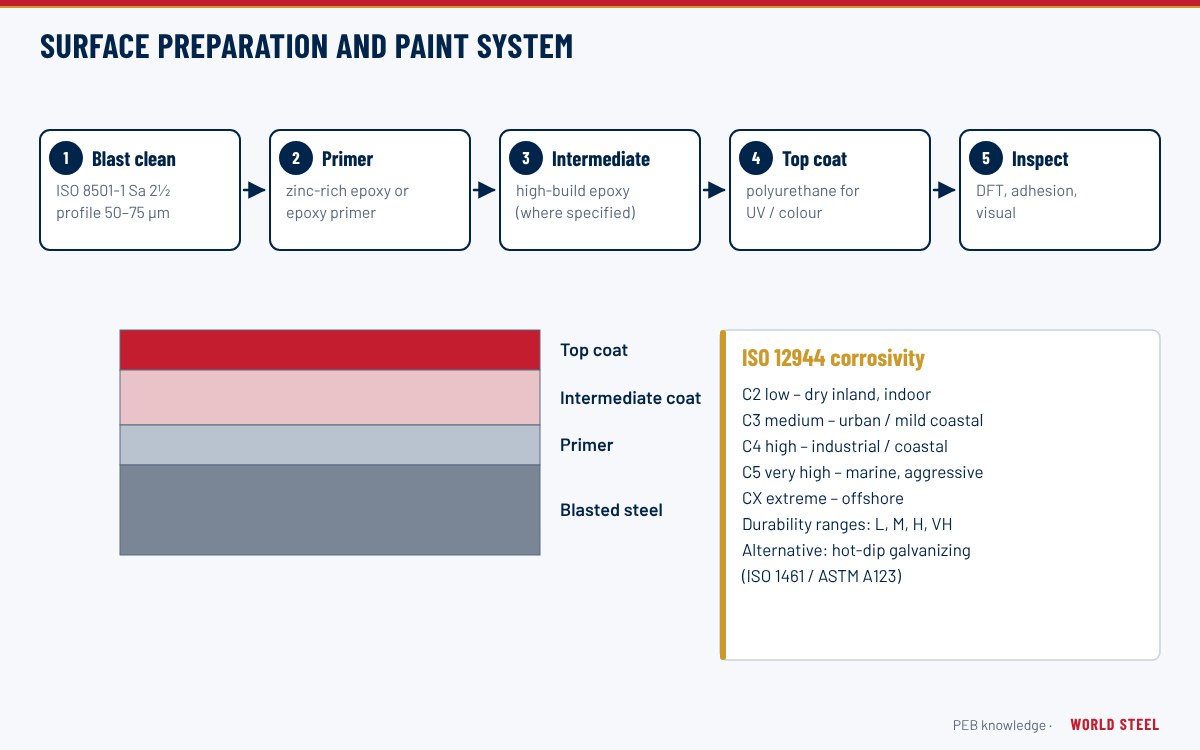
- Abrasive blast cleaning to Sa 2½ / SSPC-SP 10 in the factory
- Galvanizing, epoxy, alkyd and duplex options in one package
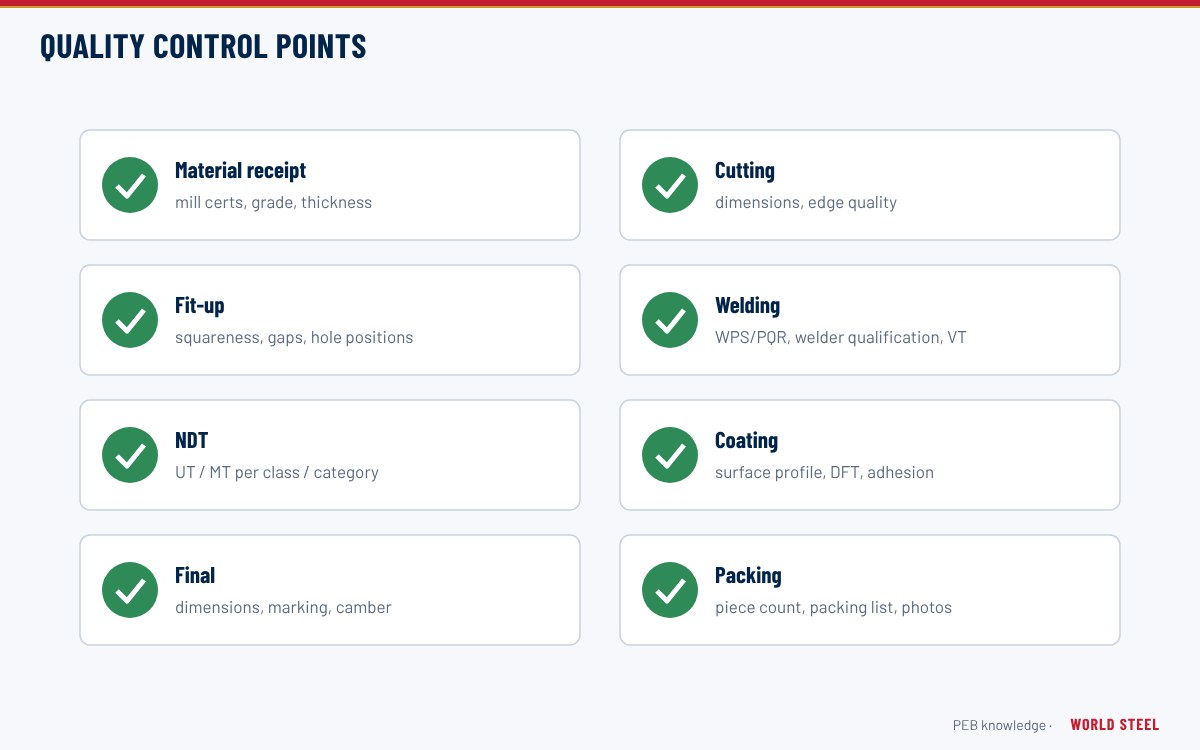
- DFT and adhesion recorded in coating inspection reports
- Specified to ISO 12944, AS/NZS 2312 and SSPC practice
Why the coating system matters
Steel corrodes wherever oxygen and moisture meet bare metal; chlorides from the sea, sulphur compounds from industry and condensation inside unventilated buildings accelerate the process. The coating system is therefore part of the structural design: it decides how long the steel keeps its section before the first major maintenance, how the building looks after ten years and how much the owner will spend on repainting. For an exported steel package the coating also has to survive handling, sea freight in containers or on flat racks, storage on site and erection damage.
World Steel applies coatings in the factory after fabrication, so the client receives steel that is ready to erect with one documented system. This page is the overview and selection guide; the individual systems are described on their own pages: hot-dip galvanizing, epoxy and polyurethane systems, alkyd systems, duplex systems, intumescent fire protection and the coating manufacturers whose systems are applied at World Steel.
Corrosivity categories and durability
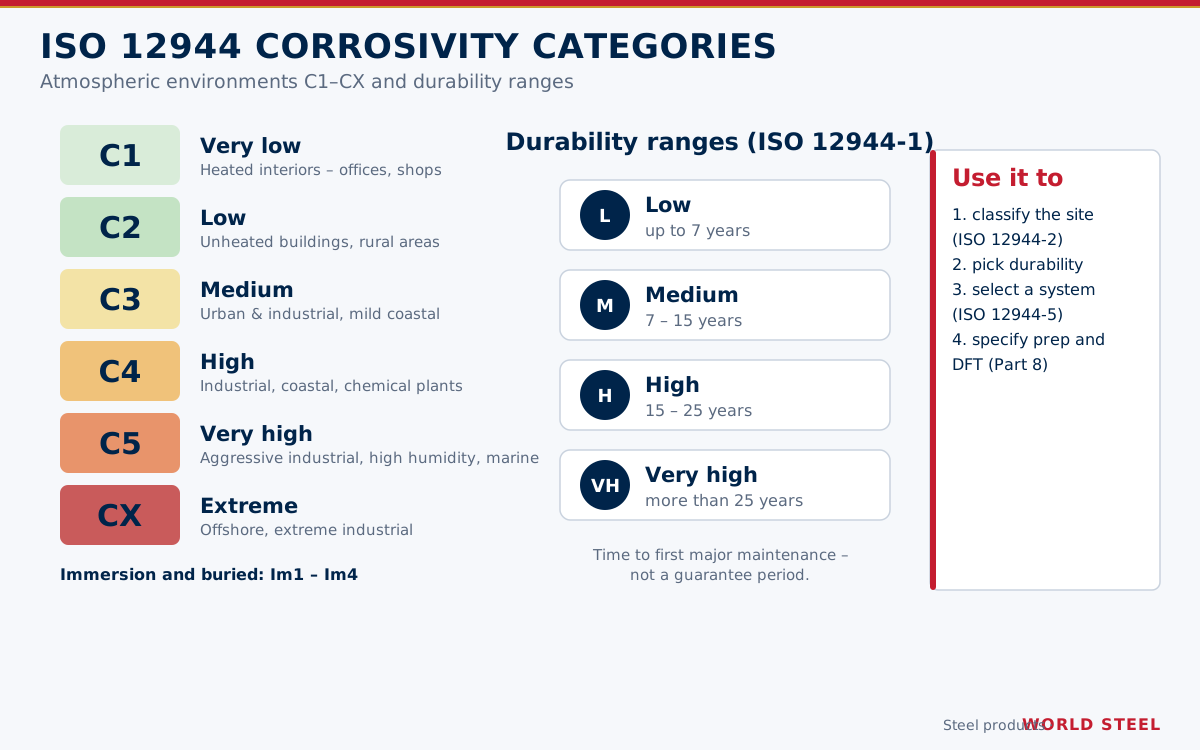
ISO 12944-2 classifies atmospheric environments from C1 very low (heated, dry interiors) through C2 low, C3 medium, C4 high and C5 very high to CX extreme (offshore and severe industrial exposure), plus immersion and buried categories Im1–Im4. The category is set by the designer from the site location, distance to the coast, industrial pollution and the micro-climate around each member – the inside of a ventilated warehouse and the eaves of the same building near the sea can fall into different categories. In Australia AS 4312 maps atmospheric corrosivity zones, and AS/NZS 2312.1 and AS/NZS 2312.2 give paint and galvanizing guidance against them.
ISO 12944-1 then defines the required durability as the time to the first major maintenance: low (L) up to 7 years, medium (M) 7–15 years, high (H) 15–25 years and very high (VH) more than 25 years. Durability is a planning figure for the owner, not a guarantee period; warranties are a separate commercial matter between the parties.
Choosing between galvanizing, epoxy, alkyd and duplex
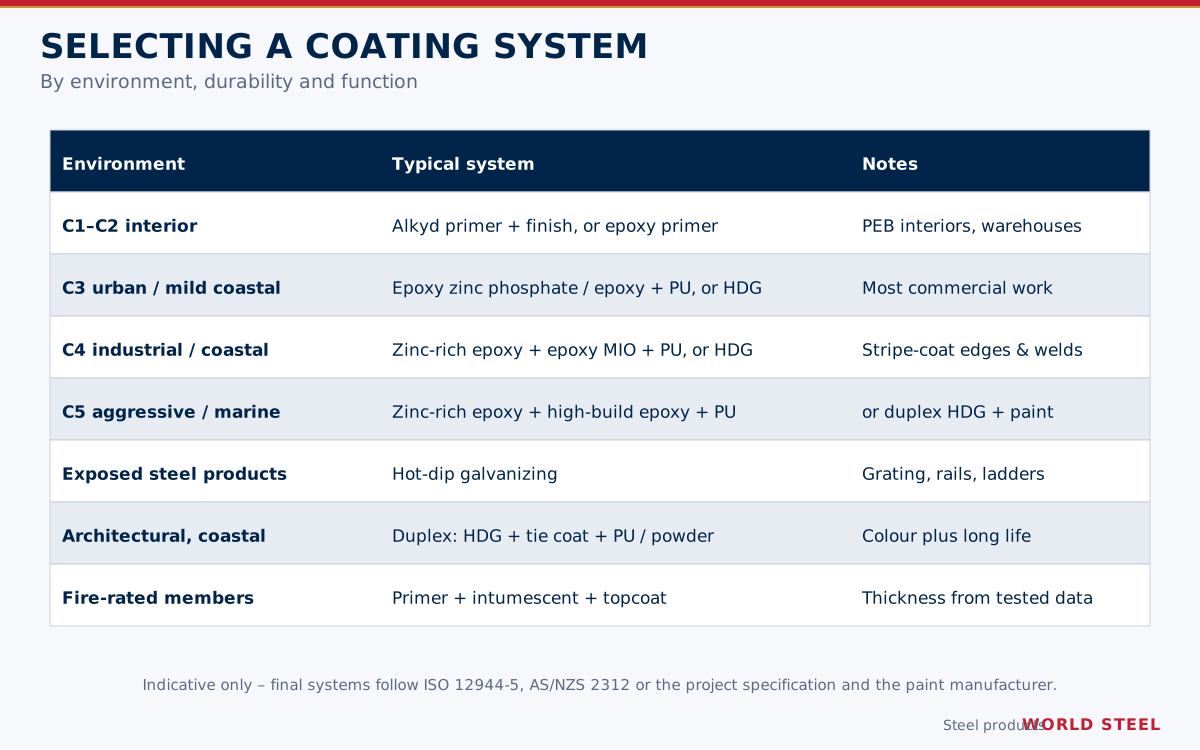
The table below is a first guide only. The final system – number of coats, generic type and nominal dry film thickness – is confirmed against ISO 12944-5 (or AS/NZS 2312.1 / 2312.2) and the coating manufacturer's recommendation for the actual category and durability.
| Environment | Corrosivity | Typical system type |
|---|---|---|
| Heated, dry building interior; PEB frames behind cladding | C1–C2 | Alkyd primer, or single epoxy primer where a longer life is needed |
| Unheated interior with condensation; rural or urban exterior | C2–C3 | Alkyd or epoxy two-coat system; hot-dip galvanizing for small items |
| Industrial or coastal exterior; plant structures | C4 | Zinc-rich epoxy / epoxy / polyurethane, or hot-dip galvanizing |
| Marine, heavy industrial, high humidity with chlorides | C5 | Multi-coat zinc-rich epoxy system of high build, galvanizing, or duplex |
| Offshore, splash zone, severe chemical exposure | CX / Im | Specialist systems to ISO 12944-9 and the owner's specification |
| Exposed architectural steel, canopies, balustrades | C3–C5 | Duplex (galvanizing + paint or powder) for colour and long life |
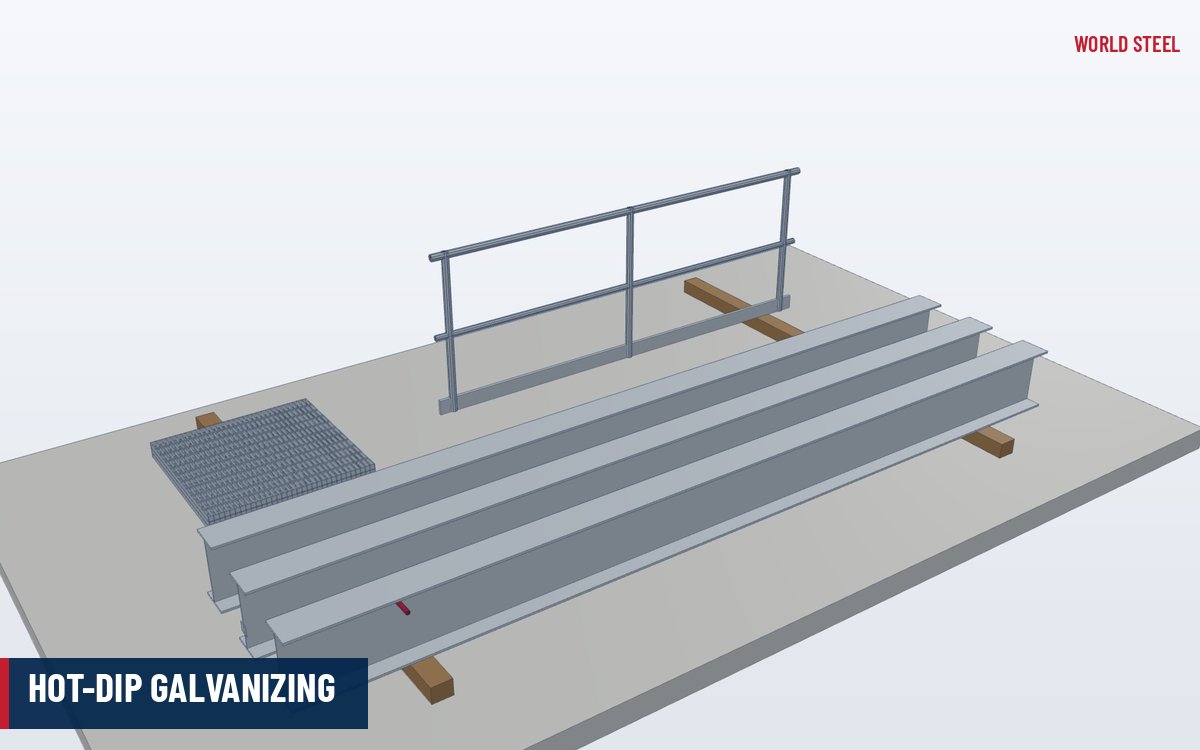
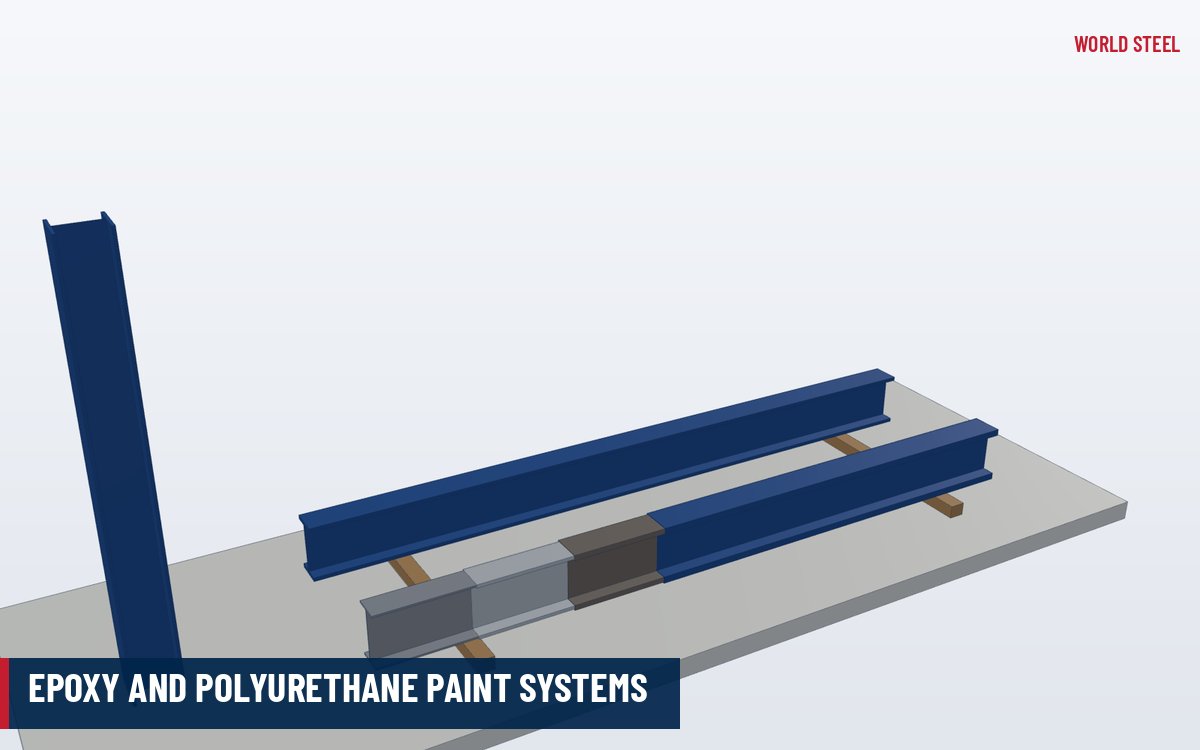
Hot-dip galvanizing suits grating, handrails, ladders and lintels; multi-coat epoxy systems suit large members that need a colour finish; alkyd is the economical answer for dry interiors; duplex combines the strengths of zinc and paint. Fire protection, where required, is added on top of a compatible anti-corrosive primer.
Surface preparation
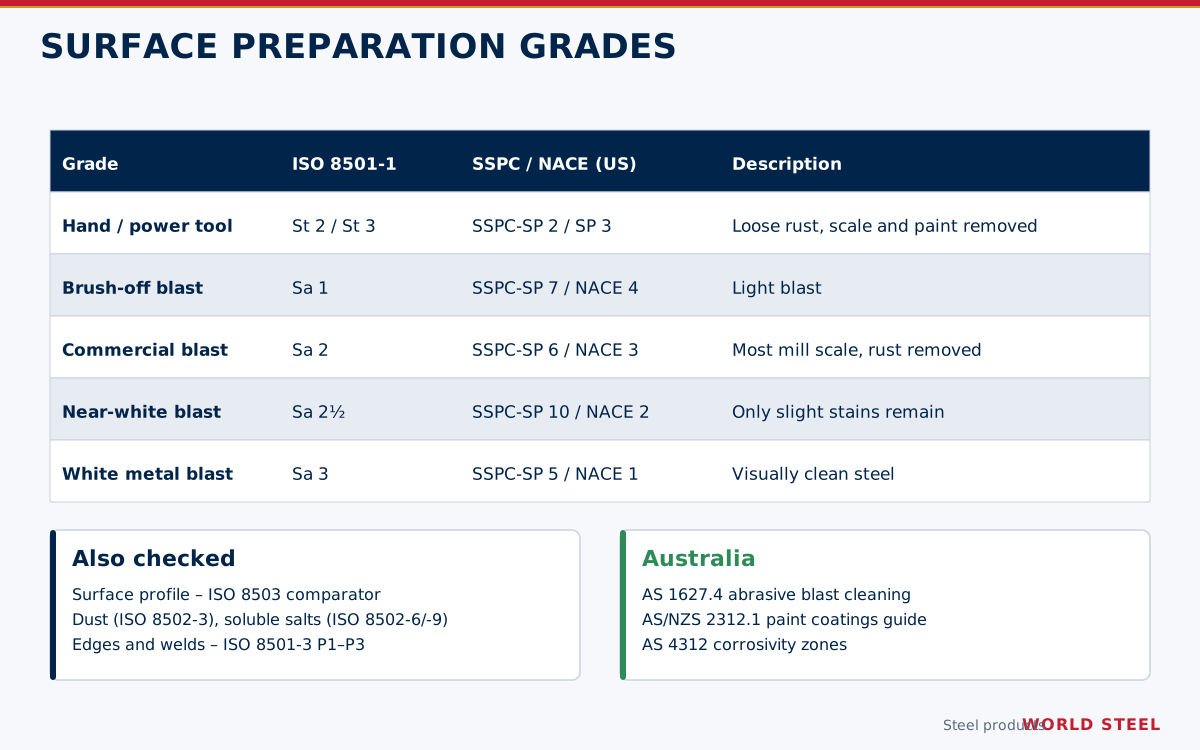
Most coating failures start at the surface. World Steel removes mill scale and rust by abrasive blast cleaning in the factory to the grade the system needs – typically Sa 2½ to ISO 8501-1 (equivalent to SSPC-SP 10 / NACE No. 2 near-white blast) for zinc-rich and epoxy primers, and Sa 2 or SSPC-SP 6 commercial blast where the specification allows. Welds, edges and imperfections are dressed to the ISO 8501-3 preparation grade (P1–P3) set by the designer, the surface profile is checked with an ISO 8503 comparator, and dust (ISO 8502-3) and soluble salts (ISO 8502-6/-9) are controlled where specified. Australian projects reference AS 1627.4 for abrasive blast cleaning. More background is in the PEB article on surface preparation and painting.
How World Steel specifies, applies and inspects
- Specify: the coating system is taken from the project specification; where the client only gives the environment and durability, World Steel proposes a system based on ISO 12944-5 and the manufacturer's data sheets for approval.
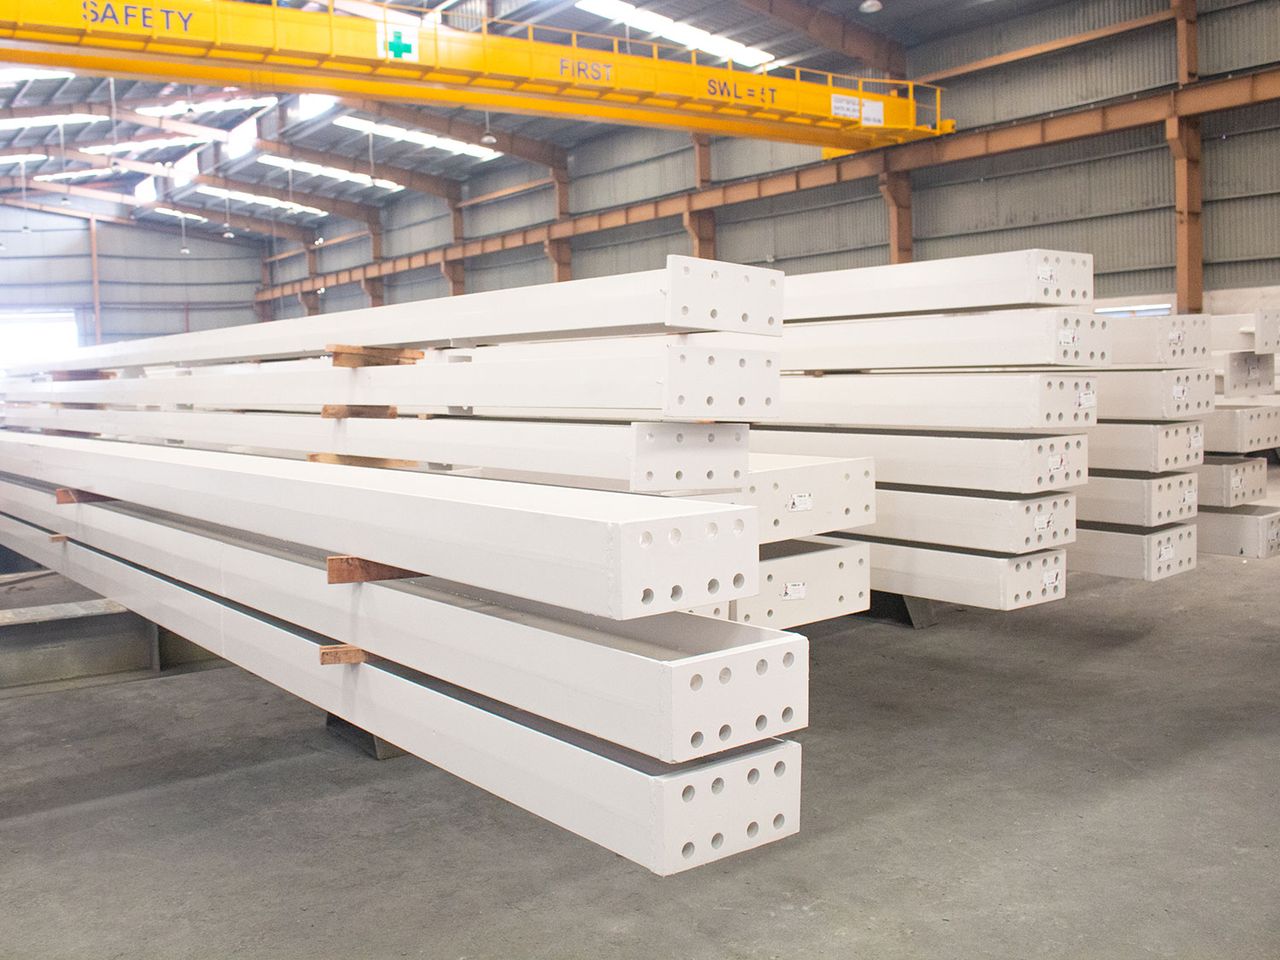
- Apply: blast cleaning and airless spray painting are carried out in the factory to the manufacturer's product data sheets – mixing, induction, temperature, humidity, dew point and overcoating intervals – with stripe coats on edges and welds.
- Inspect: dry film thickness is measured to ISO 19840 / ISO 2808 or SSPC-PA 2, adhesion is checked by pull-off (ISO 4624 / ASTM D4541) or cross-cut (ISO 2409 / ASTM D3359) where specified, and results are recorded in the coating inspection report.
- Protect: coated steel is packed with dunnage and edge protection for export; touch-up paint and repair procedures are supplied for site damage.
Coating work is part of execution under AS/NZS 5131 and EN 1090-2, both of which World Steel is certified to; see also the PEB article on paint and coating systems.
Norme e requisiti per mercato
I codici secondo cui World Steel progetta, fabbrica e documenta questo prodotto, con i principali requisiti geometrici e di carico in ciascun mercato.
 Stati Uniti
- SSPC-SP 10 / NACE No. 2Near-white metal blast cleaning
- SSPC-SP 6 / NACE No. 3Commercial blast cleaning
- SSPC-PA 2Measurement of dry coating thickness with magnetic gauges
- ASTM A123Zinc (hot-dip galvanized) coatings on iron and steel products
- ASTM A780Repair of damaged and uncoated areas of hot-dip galvanized coatings
- ASTM D4541Pull-off strength of coatings using portable adhesion testers
- Surface preparation for zinc-rich primers
- SSPC-SP 10 / NACE No. 2 near-white blast (typical, per data sheet)
- Dry film thickness
- Measured and accepted per SSPC-PA 2
- Galvanizing repair
- Zinc-rich paint, spray or solder per ASTM A780
 Australia / NZ
- AS/NZS 2312.1Guide to the protection of structural steel – paint coatings
- AS/NZS 2312.2Guide to the protection of structural steel – hot-dip galvanizing
- AS 4312Atmospheric corrosivity zones in Australia
- AS 1627.4Abrasive blast cleaning of steel
- AS/NZS 4680Hot-dip galvanized coatings on fabricated ferrous articles
- AS/NZS 5131 Certificata WSCFabrication and erection of structural steelwork
- Corrosivity
- Zone per AS 4312, system per AS/NZS 2312.1 / 2312.2
- HDG on steel > 6 mm
- 600 g/m² (85 µm) average (AS/NZS 4680)
 Europa
- EN ISO 12944-2Classification of environments C1–CX, Im1–Im4
- EN ISO 12944-5Protective paint systems
- EN ISO 8501-1Rust grades and preparation grades of uncoated steel
- EN ISO 8501-3Preparation grades of welds, edges and imperfections
- EN ISO 1461Hot-dip galvanized coatings on fabricated articles
- EN ISO 19840Measurement of DFT on rough surfaces
- EN 1090-2 Certificata WSCExecution of steel structures – technical requirements
- Surface preparation for paint systems
- Sa 2½ (EN ISO 8501-1), typical
- Durability
- L ≤ 7 y, M 7–15 y, H 15–25 y, VH > 25 y to first major maintenance (EN ISO 12944-1)
- Min. HDG thickness > 6 mm steel
- 85 µm mean, 70 µm local (EN ISO 1461)
Sintesi solo orientativa: prevalgono il capitolato di progetto, l'edizione del codice adottata e l'autorità competente.
Finiture
| Finitura | Norme / note |
|---|---|
| Hot-dip galvanized | ASTM A123 · AS/NZS 4680 · EN ISO 1461 |
| Epoxy / polyurethane paint system | SSPC-SP 10 + SSPC-PA 2 · AS/NZS 2312.1 · EN ISO 12944-5 |
| Alkyd paint system | SSPC-SP 6 / SP 10 · AS/NZS 2312.1 · EN ISO 12944-5 (C1–C3) |
| Duplex (galvanized + paint) | ASTM A123 + ASTM D6386 · AS/NZS 4680 + AS/NZS 2312.1 · EN ISO 1461 + EN ISO 12944 |
Domande frequenti
Which corrosivity category applies to my project?
The category is set by the designer from the site and the exposure of each member, using ISO 12944-2 (or AS 4312 in Australia). If it is not stated, send the location and a description of the environment and World Steel will propose a system for approval.
Is the ISO 12944 durability a guarantee?
No. ISO 12944-1 durability (L, M, H, VH) is the expected time to the first major maintenance and is used to select a system. Any warranty is a separate commercial agreement.
Should I galvanize or paint?
Galvanizing is usually best for grating, handrails, ladders and smaller items in C3–C5 exposure; paint systems suit large members needing a colour finish; duplex gives the longest life for exposed architectural steel. The final choice depends on durability, appearance, member size and cost.
How is coating quality checked?
Surface preparation, ambient conditions, dry film thickness and, where specified, adhesion are checked in the factory and recorded in the coating inspection report supplied with the steel.
 Singapore
 AS/NZS 5131 CC3
 EN 1090 EXC3 · CE
 IAS AC472