ENEnglish
 VITiếng Việt
 ZH中文
 KO한국어
 JA日本語
 FRFrançais
 ITItaliano
 PTPortuguês
 ESEspañol
 HEעברית
 ARالعربية

Fit-up of web and flanges
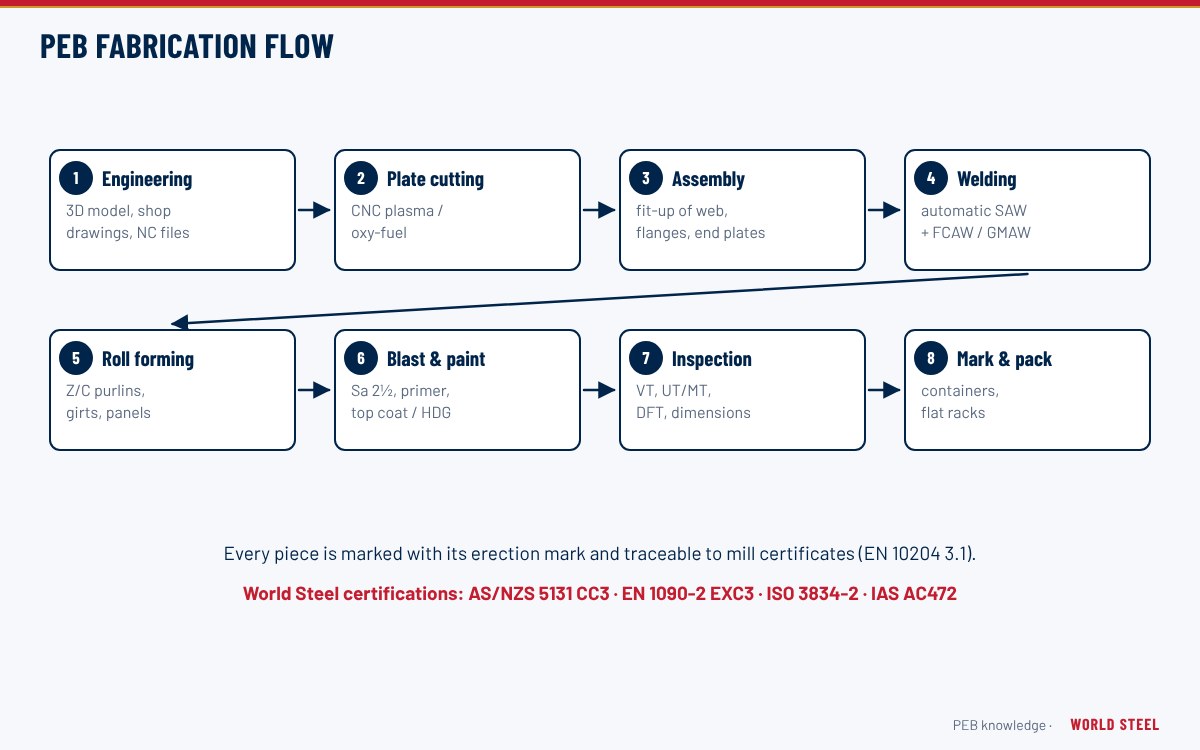
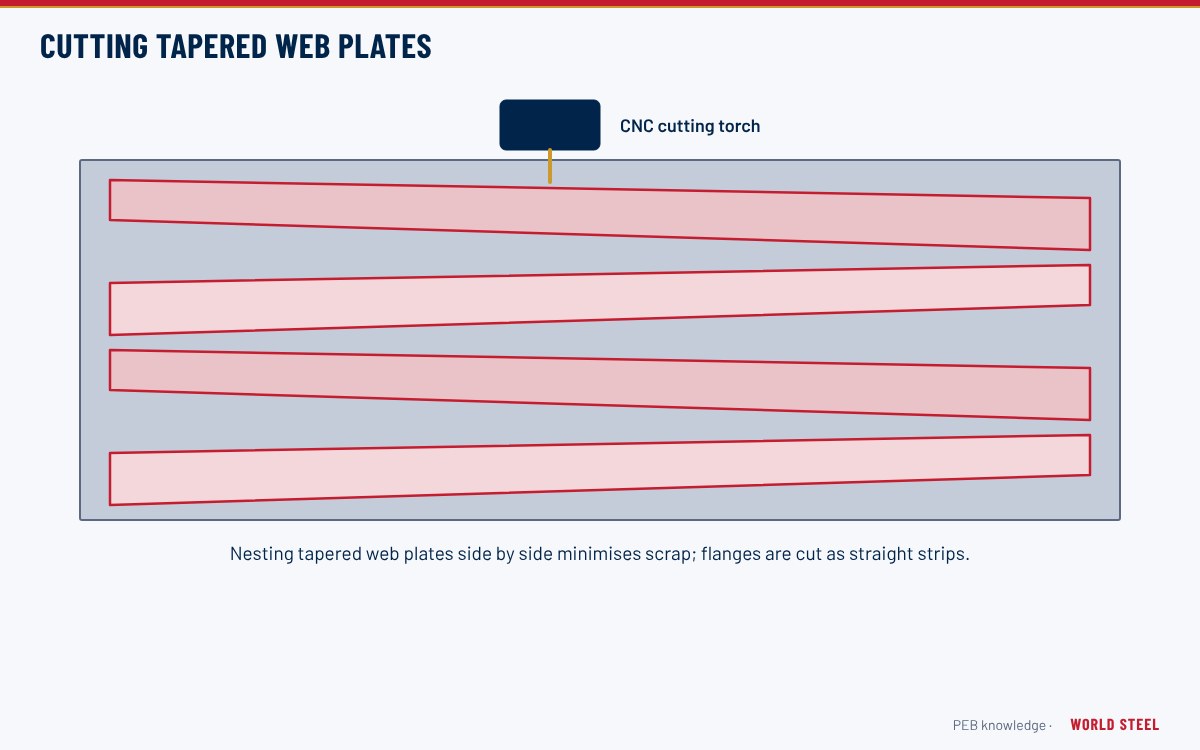
After plate cutting, each tapered web is assembled with its two flanges into an I-section. Fit-up is done on an H-beam assembly machine or a fit-up table that centres the web on the flange, holds it square and closes the root gap before tack welding. Good fit-up is the precondition for good automatic welding: a gap at the flange-to-web joint wastes consumable, increases distortion and can cause lack of fusion.
Tack welds are made with a qualified procedure, are small enough to be fully consumed by the subsequent weld and must be free of cracks. Run-on and run-off tabs may be added at member ends so that the arc starts and stops outside the finished member.
Submerged arc welding (SAW)
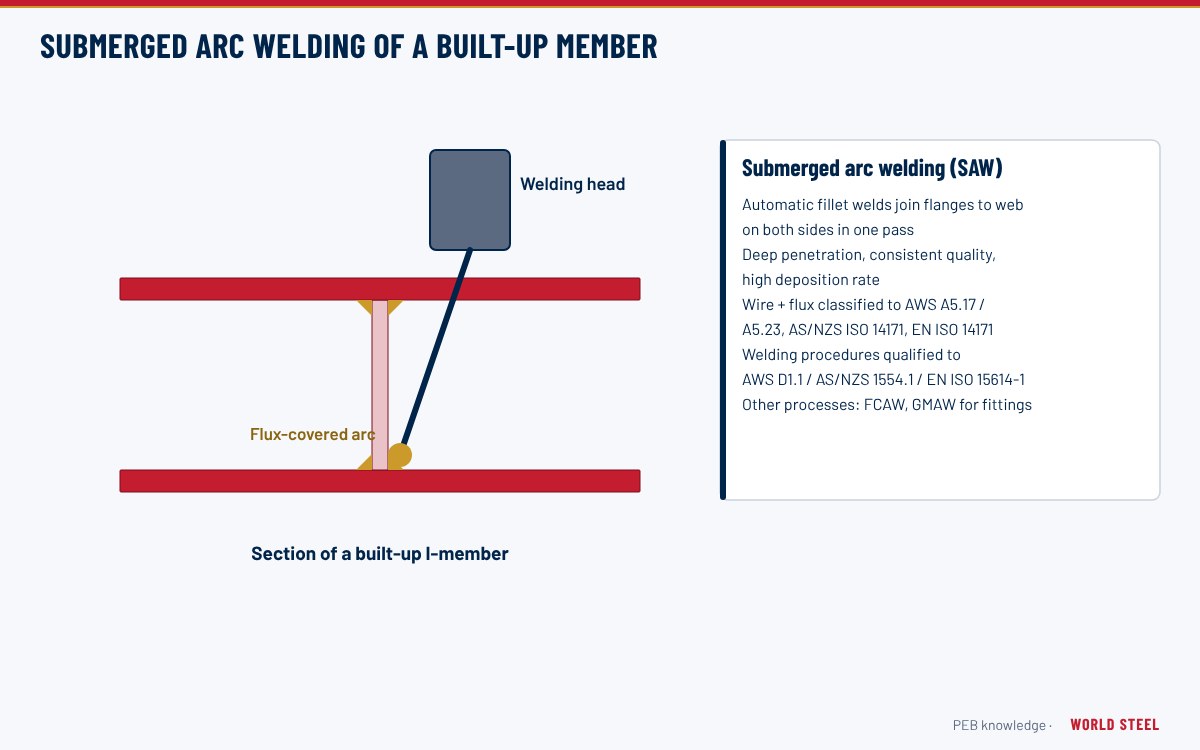
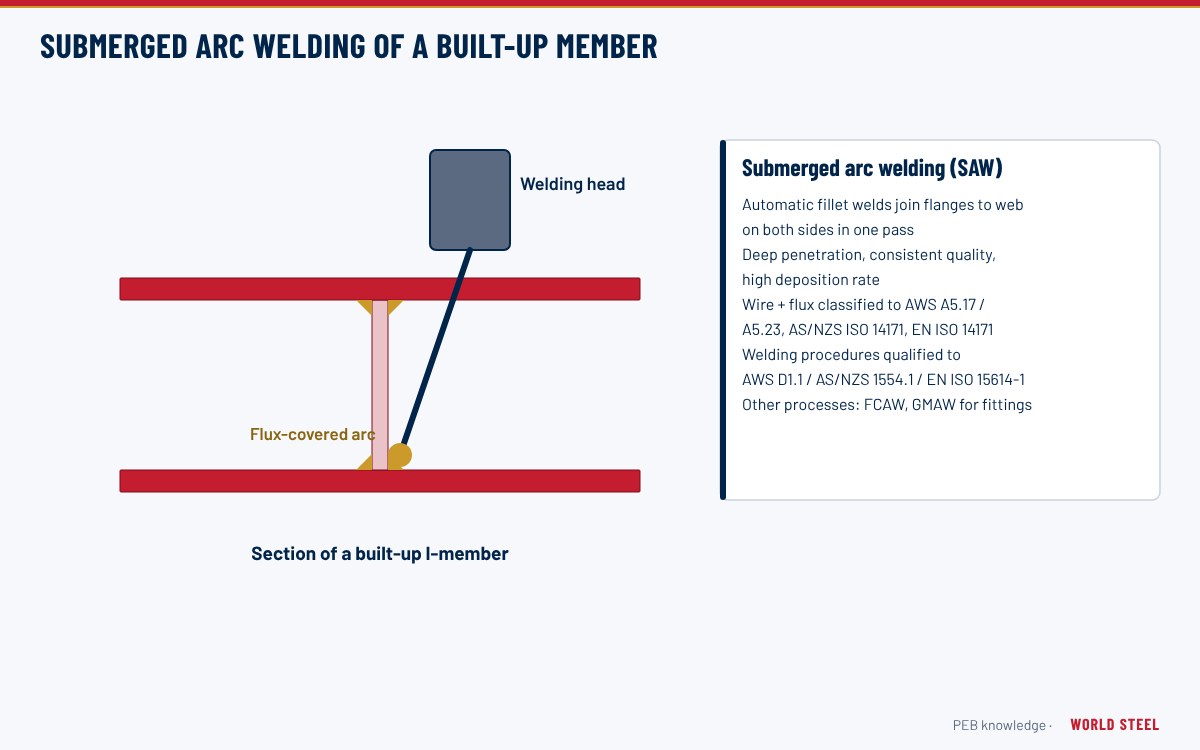
The flange-to-web joints are long, continuous fillet welds – exactly the kind of joint where submerged arc welding excels. The arc burns under a blanket of granular flux, which shields the weld pool, gives deep penetration and a smooth bead and eliminates arc glare and spatter. Typical PEB lines use gantry or cantilever machines with one or two heads, welding both fillets on one side simultaneously while the member is held in a positioner, then rotating the member to weld the opposite flange. Tandem-wire or twin-wire heads increase deposition for heavy crane girders.
| Process | Typical PEB application | Notes |
|---|---|---|
| SAW (submerged arc) | Flange-to-web fillets of columns, rafters, crane girders | High deposition, mechanised, low defect rate |
| FCAW (flux-cored) | End plates, stiffeners, base plates, cleats | All-position, good productivity for short welds |
| GMAW (solid wire, CO2 / mixed gas) | Light secondary fabrication, brackets, tack welds | Fast and clean in shop conditions |
| SMAW (stick) | Repairs and site welding | Flexible, slower |
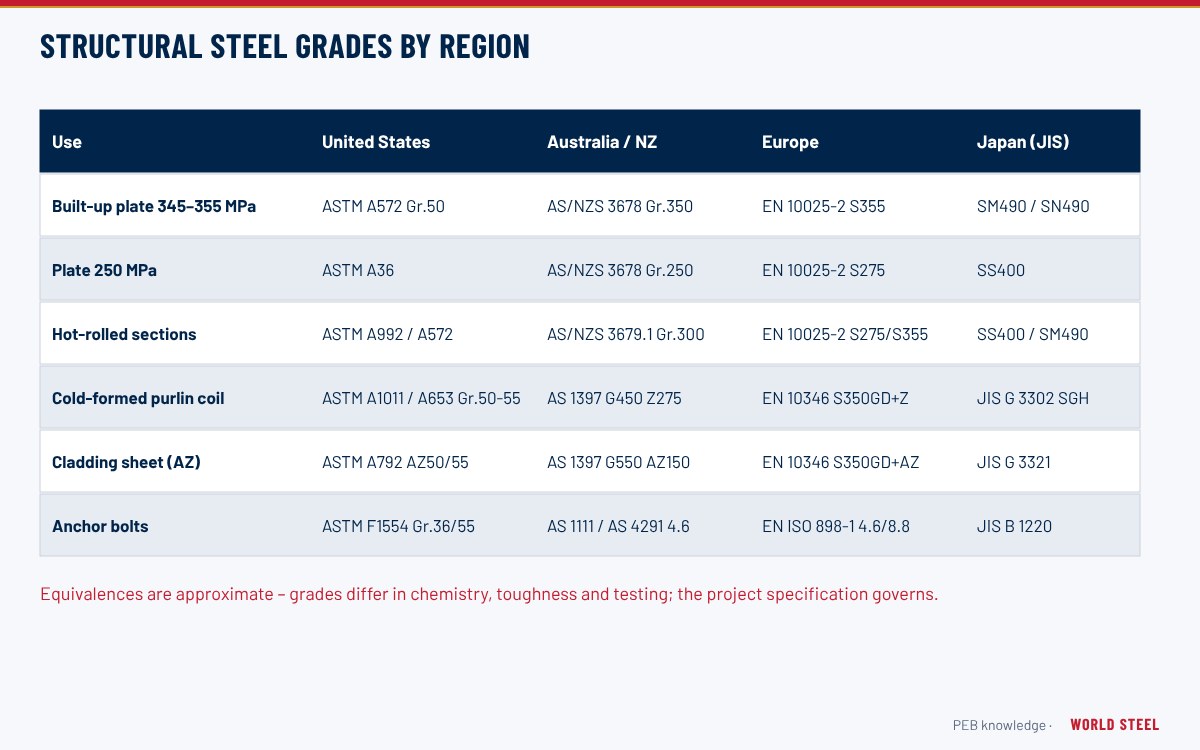
Consumables are matched to the parent steel: for example AWS A5.17 wire/flux classifications such as F7A2-EM12K for ASTM A572 Grade 50 plate, or ISO 14171 wire/flux classifications for AS/NZS 3678 Grade 350 and EN 10025-2 S355 plate. See welding processes and consumables.
Weld size and procedure qualification
For most PEB frames the flange-to-web weld is a fillet on both sides; full-penetration welds are needed only at specific locations such as heavily loaded knees or where the design requires it. Every weld is made to a qualified welding procedure specification (WPS) – prequalified or qualified by test under AWS D1.1, AS/NZS 1554.1 or ISO 15614-1 – and by welders and operators qualified to AWS D1.1, AS/NZS 2980 or ISO 9606-1 / ISO 14732. Welding coordination personnel under ISO 14731 supervise the work in an ISO 3834-2 system.
- Preheat according to the carbon equivalent and plate thickness
- Correct wire diameter, current, voltage and travel speed as recorded in the WPS
- Dry, properly stored flux; recycled flux screened and kept within specification
- Control of distortion by welding sequence and balanced heat input
Straightening and secondary welding
Fillet welds shrink and pull the flanges into a slight umbrella shape (flange tilt) and may cause camber or sweep. Flange straightening machines roll the flange flat again; sweep is corrected by heat straightening within the temperature limits of the steel grade. The member then moves to secondary fabrication, where end plates, stiffeners, purlin clips and base plates are fitted and welded, usually by FCAW. End plates must be square and flat for the bolted connection to bear evenly, so they are checked with a square and straight edge before release.
Weld quality levels and common defects
Acceptance criteria for weld imperfections are set by the governing code: AWS D1.1 visual and NDT acceptance tables for statically and cyclically loaded connections in North America, the GP and SP weld categories of AS/NZS 1554.1 in Australia and New Zealand, and ISO 5817 quality levels (D, C, B) linked to the execution class under EN 1090-2 in Europe – level B is generally required for EXC3 work, with additional requirements for fatigue details.
| Defect | Typical cause | Prevention |
|---|---|---|
| Undersize fillet | Travel speed too high, wire misaligned to the joint | Parameter control per WPS; gauge checks at start of each member |
| Undercut | Excessive current or voltage, wrong torch angle | Correct parameters and head position |
| Porosity | Damp flux, rust or primer on the joint, gas disturbance | Dry flux, clean joint faces, draught control |
| Lack of fusion | Root gap, low heat input, poor fit-up | Tight fit-up, qualified parameters |
| Cracking | Hydrogen, restraint, high carbon equivalent, cold plate | Low-hydrogen consumables, preheat where required |
| Burn-through on thin webs | Excessive heat input on 4–6 mm plates | Reduced current, correct electrode stick-out and travel speed |
Because SAW parameters are mechanised, a defect is usually systematic rather than random: if one member shows undersize welds, the whole batch made with the same settings is checked. Recording welding parameters per member or per shift makes such checks quick and supports traceability in the quality dossier.
Inspection and WSC capability
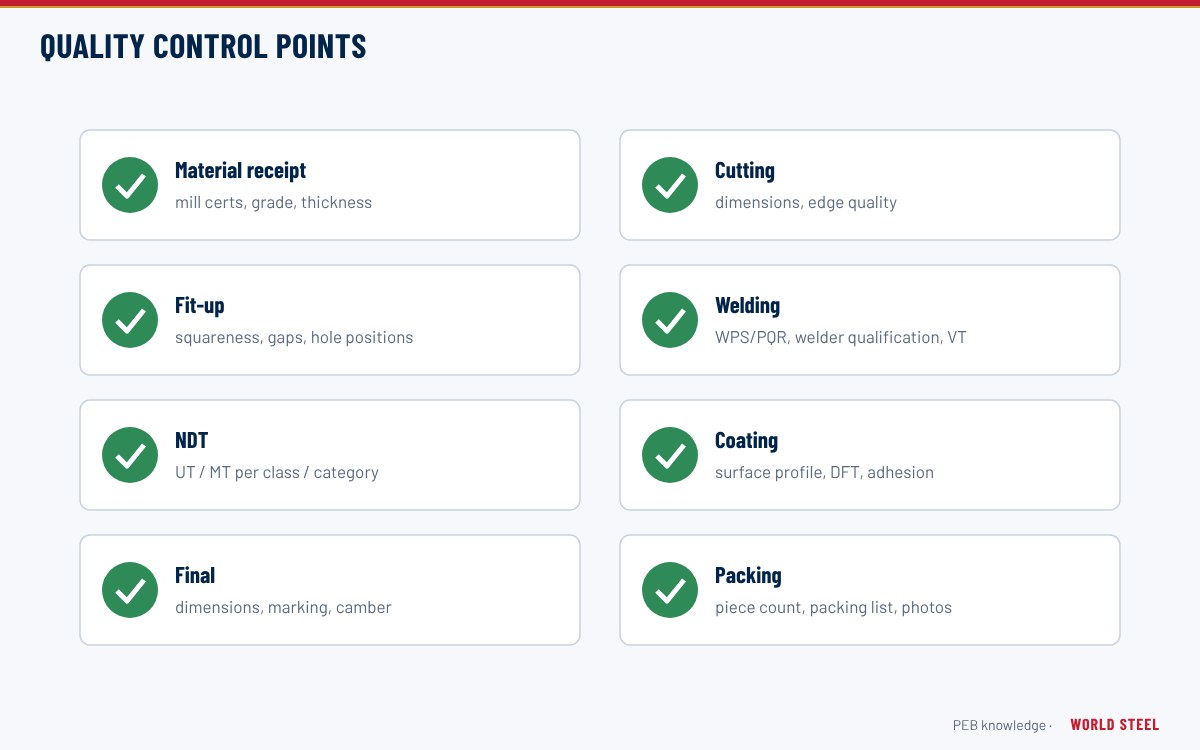
Welds are visually inspected on 100% of their length and supplemented by MT and UT to the extent required by the governing standard and execution class – see quality control and inspection. World Steel welds PEB members on automatic SAW lines under an ISO 3834-2 certified system, fabricating to EN 1090-2 EXC3 and AS/NZS 5131 CC3, with IAS AC472 accreditation for metal building systems. This capability supports both primary frame supply and heavier structural steel work.
Standards by region
| Region | Code | Scope |
|---|---|---|
 United States |
AWS D1.1 | Structural welding code – steel |
 Canada |
CSA W59 | Welded steel construction (W47.1 certification as market requirement) |
 Australia / NZ |
AS/NZS 1554.1 | Structural steel welding – welding of steel structures |
 Europe |
EN 1090-2 / EN ISO 15614-1 | Execution of steel structures; welding procedure qualification |
| International | ISO 3834-2 / ISO 9606-1 | Welding quality requirements; welder qualification |
Frequently asked questions
Why is submerged arc welding used for PEB members?
The flange-to-web joint is a long, straight, continuous weld. SAW deposits metal quickly with deep penetration and consistent quality, and it is easily mechanised on gantry lines.
Are flange-to-web welds full penetration?
Usually not. Most PEB members use double-sided fillet welds sized by the design shear flow; full-penetration welds are specified only where the engineer requires them.
How is distortion from welding corrected?
Flange tilt is corrected on flange straightening machines and camber or sweep by controlled heat straightening, within limits set by the steel grade and the fabrication standard.